Home / Services

Gear cutting, CNC machining & EDM services

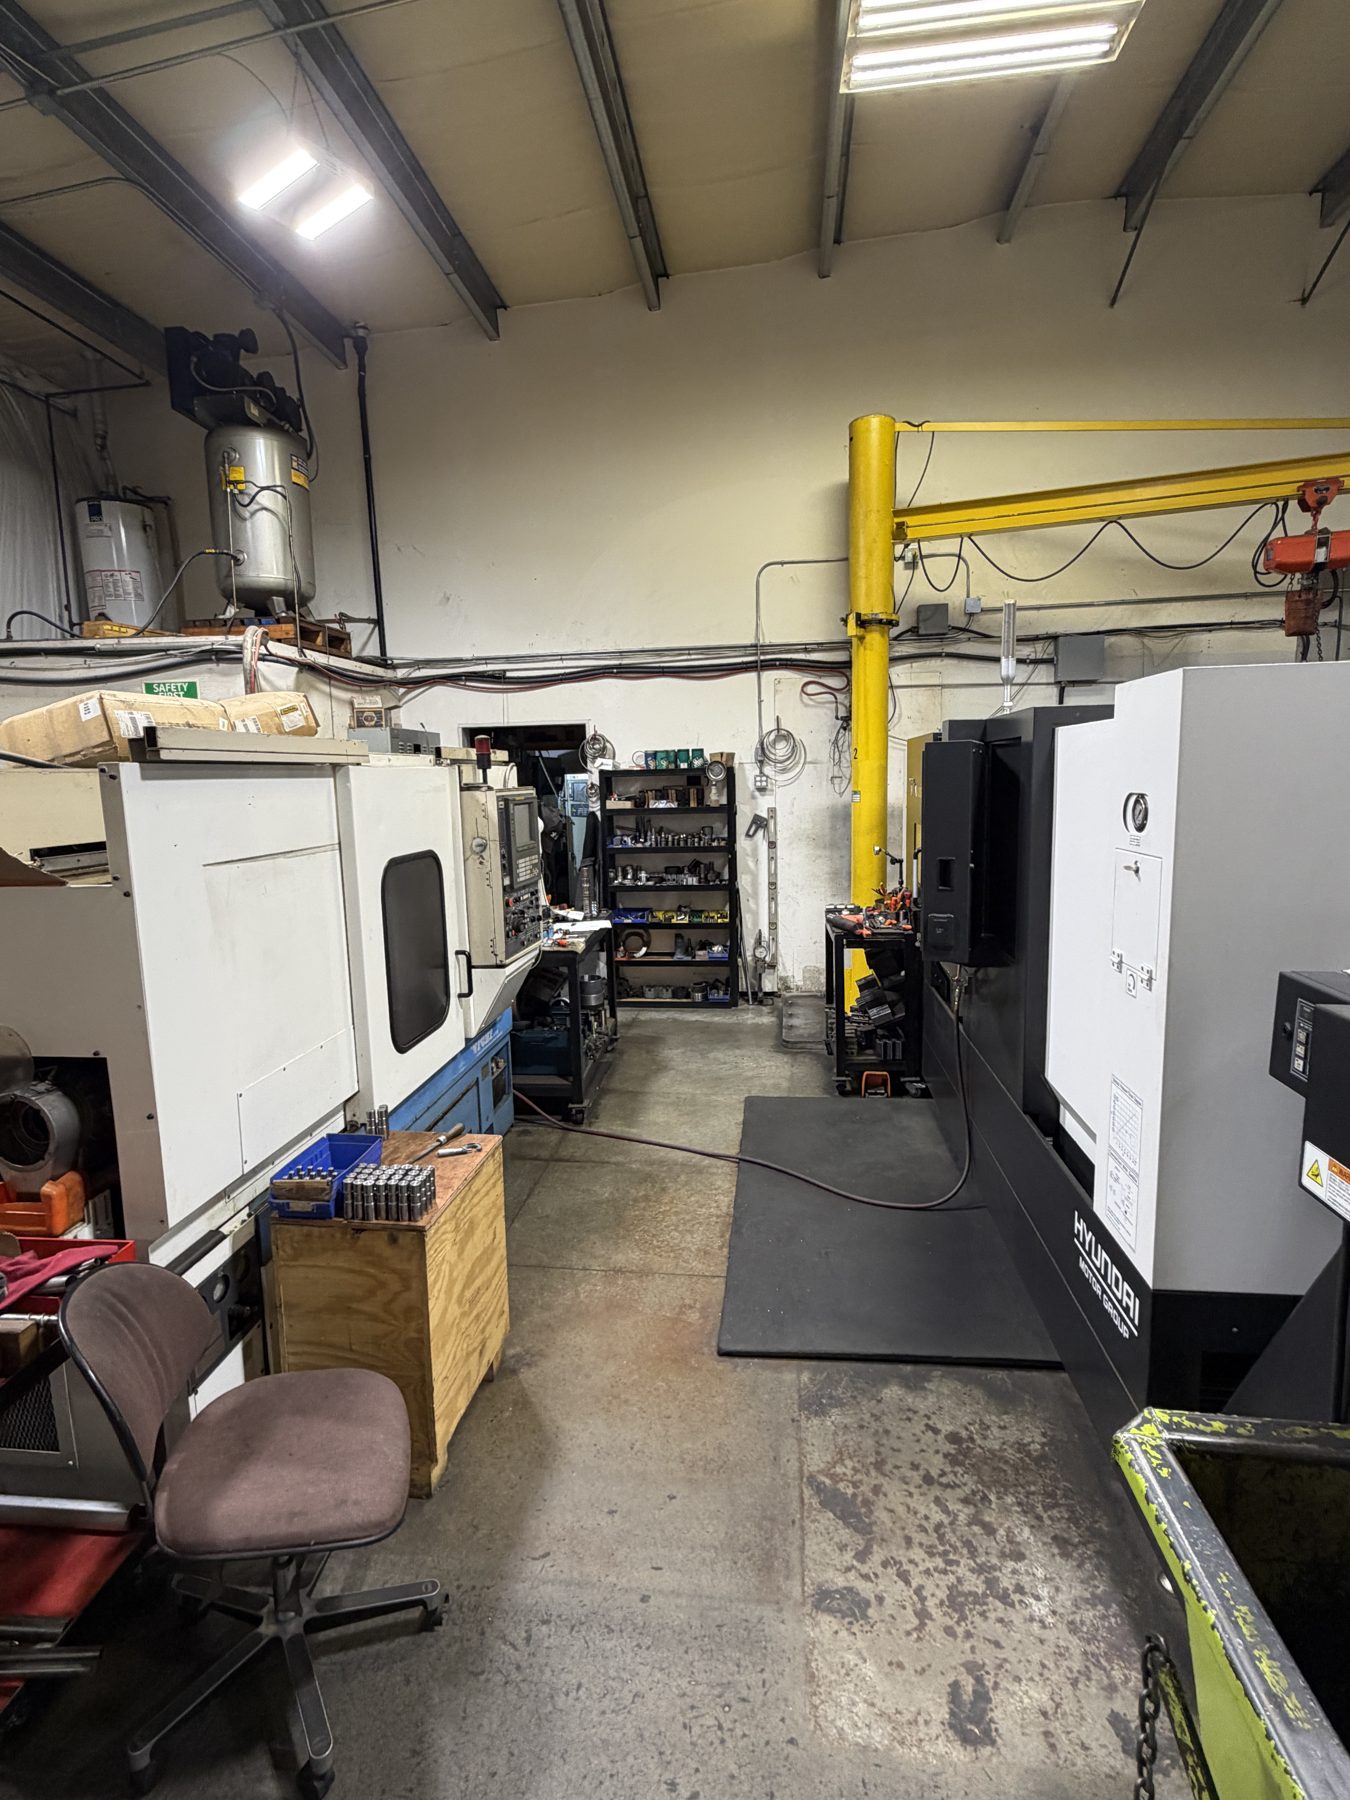
Gear cutting is our specialty, but most jobs that come through our Leduc machine shop use more than one process. Here's everything we do in-house for customers in Edmonton, Nisku and across Alberta.

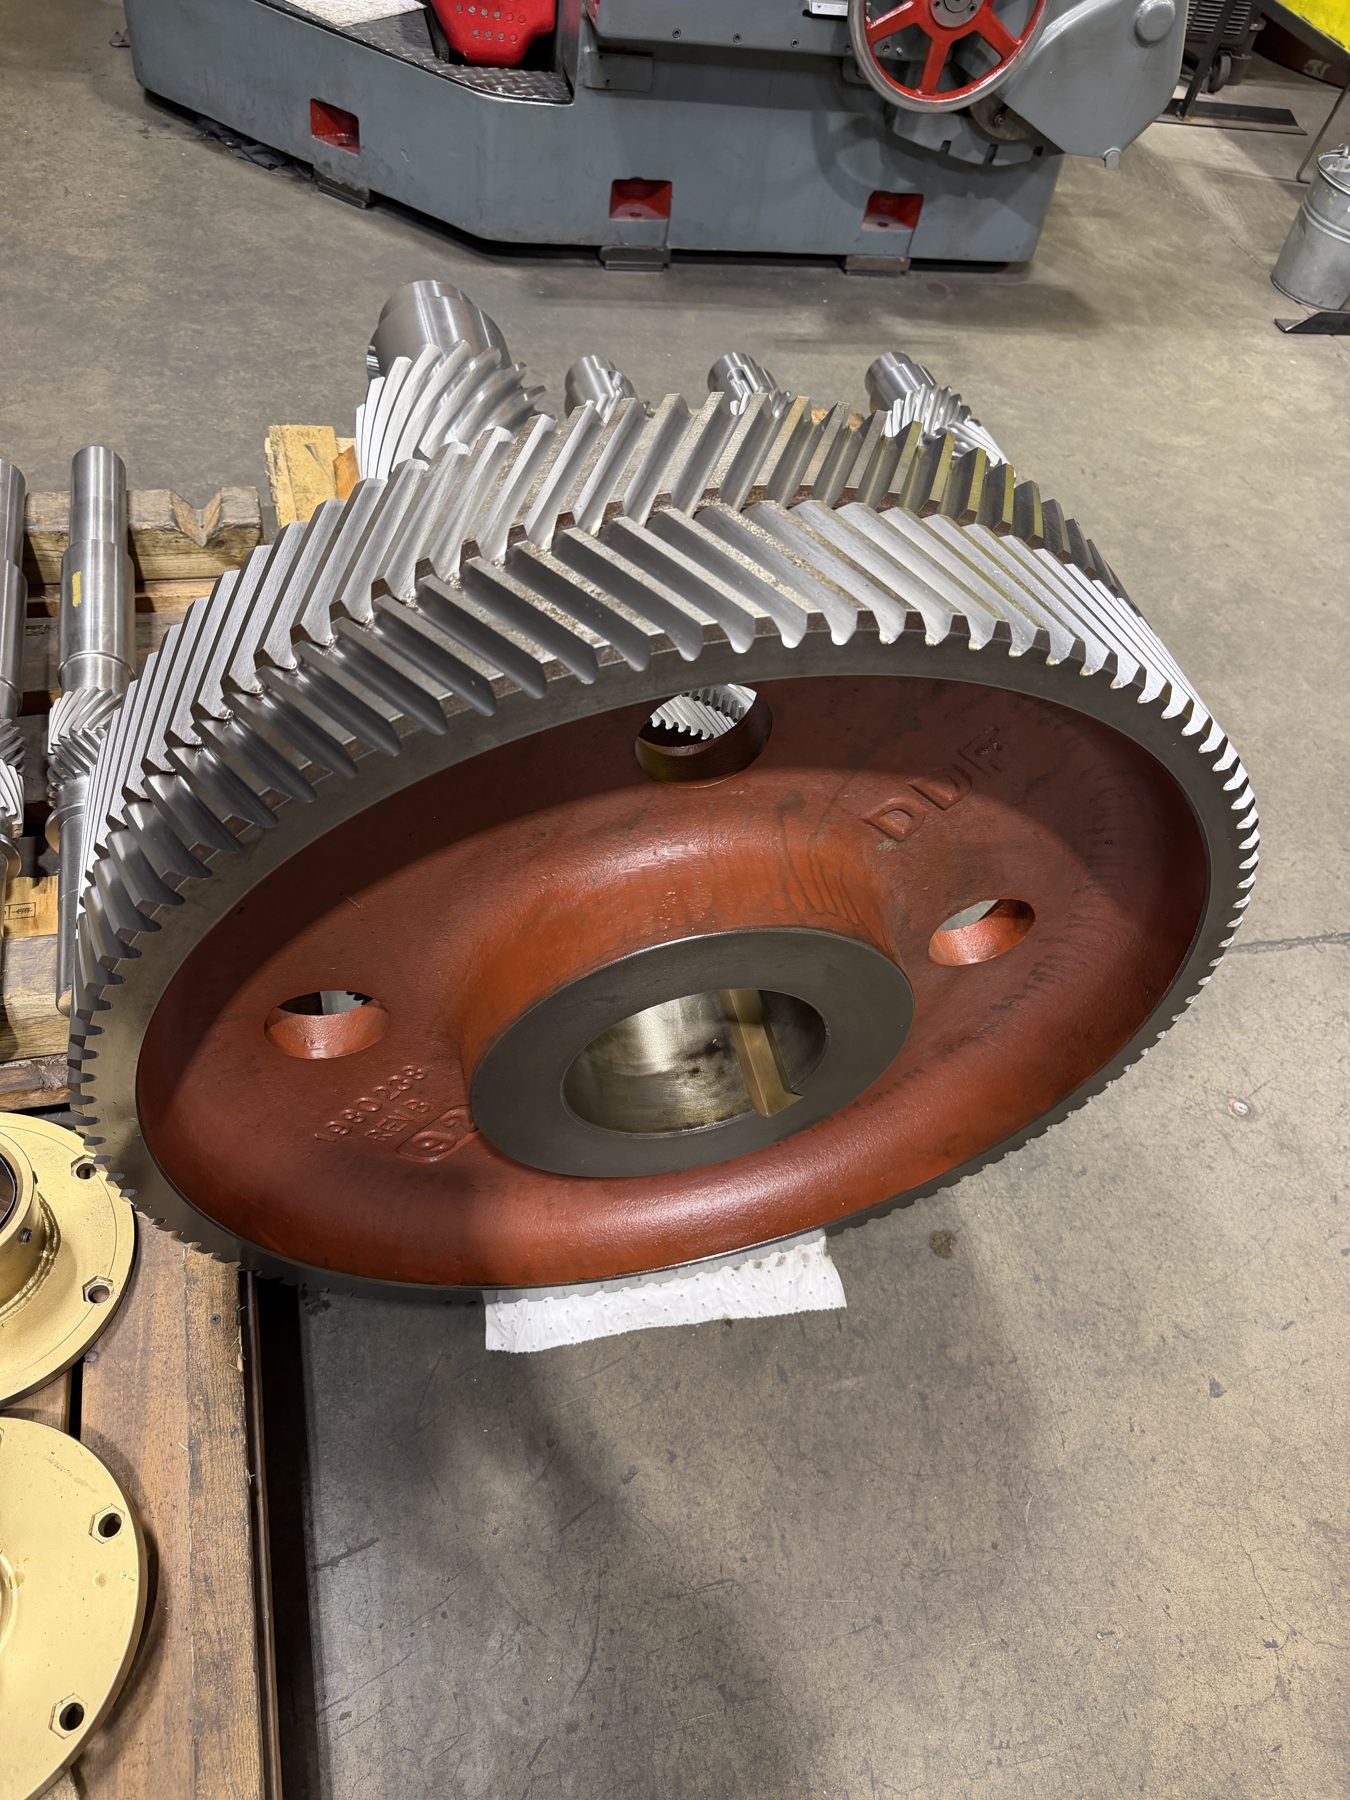
Herringbone bull gear
HerringboneSolid-apex bull gear
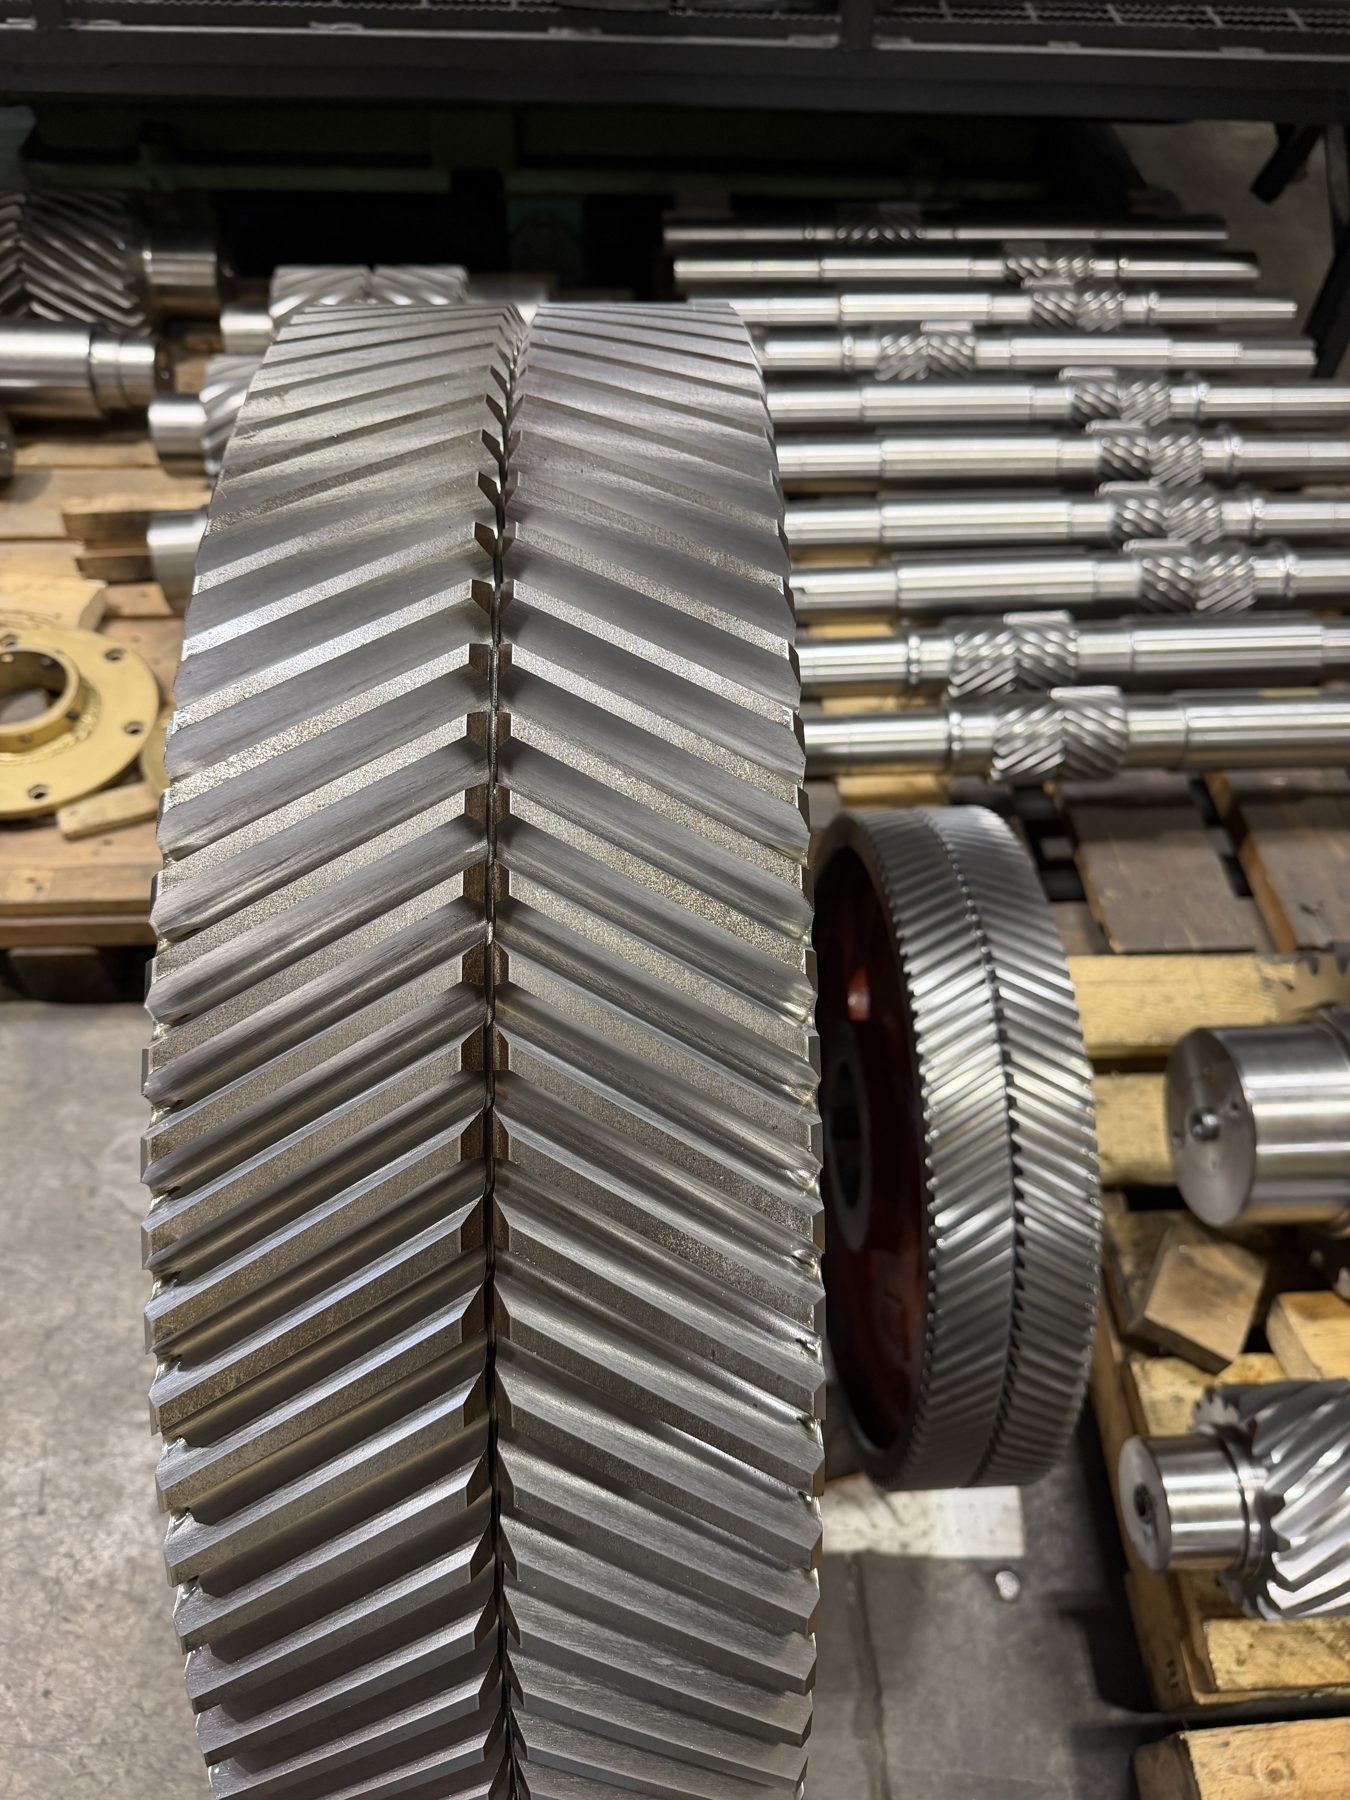
Herringbone teeth
Close-upContinuous apex, no centre groove
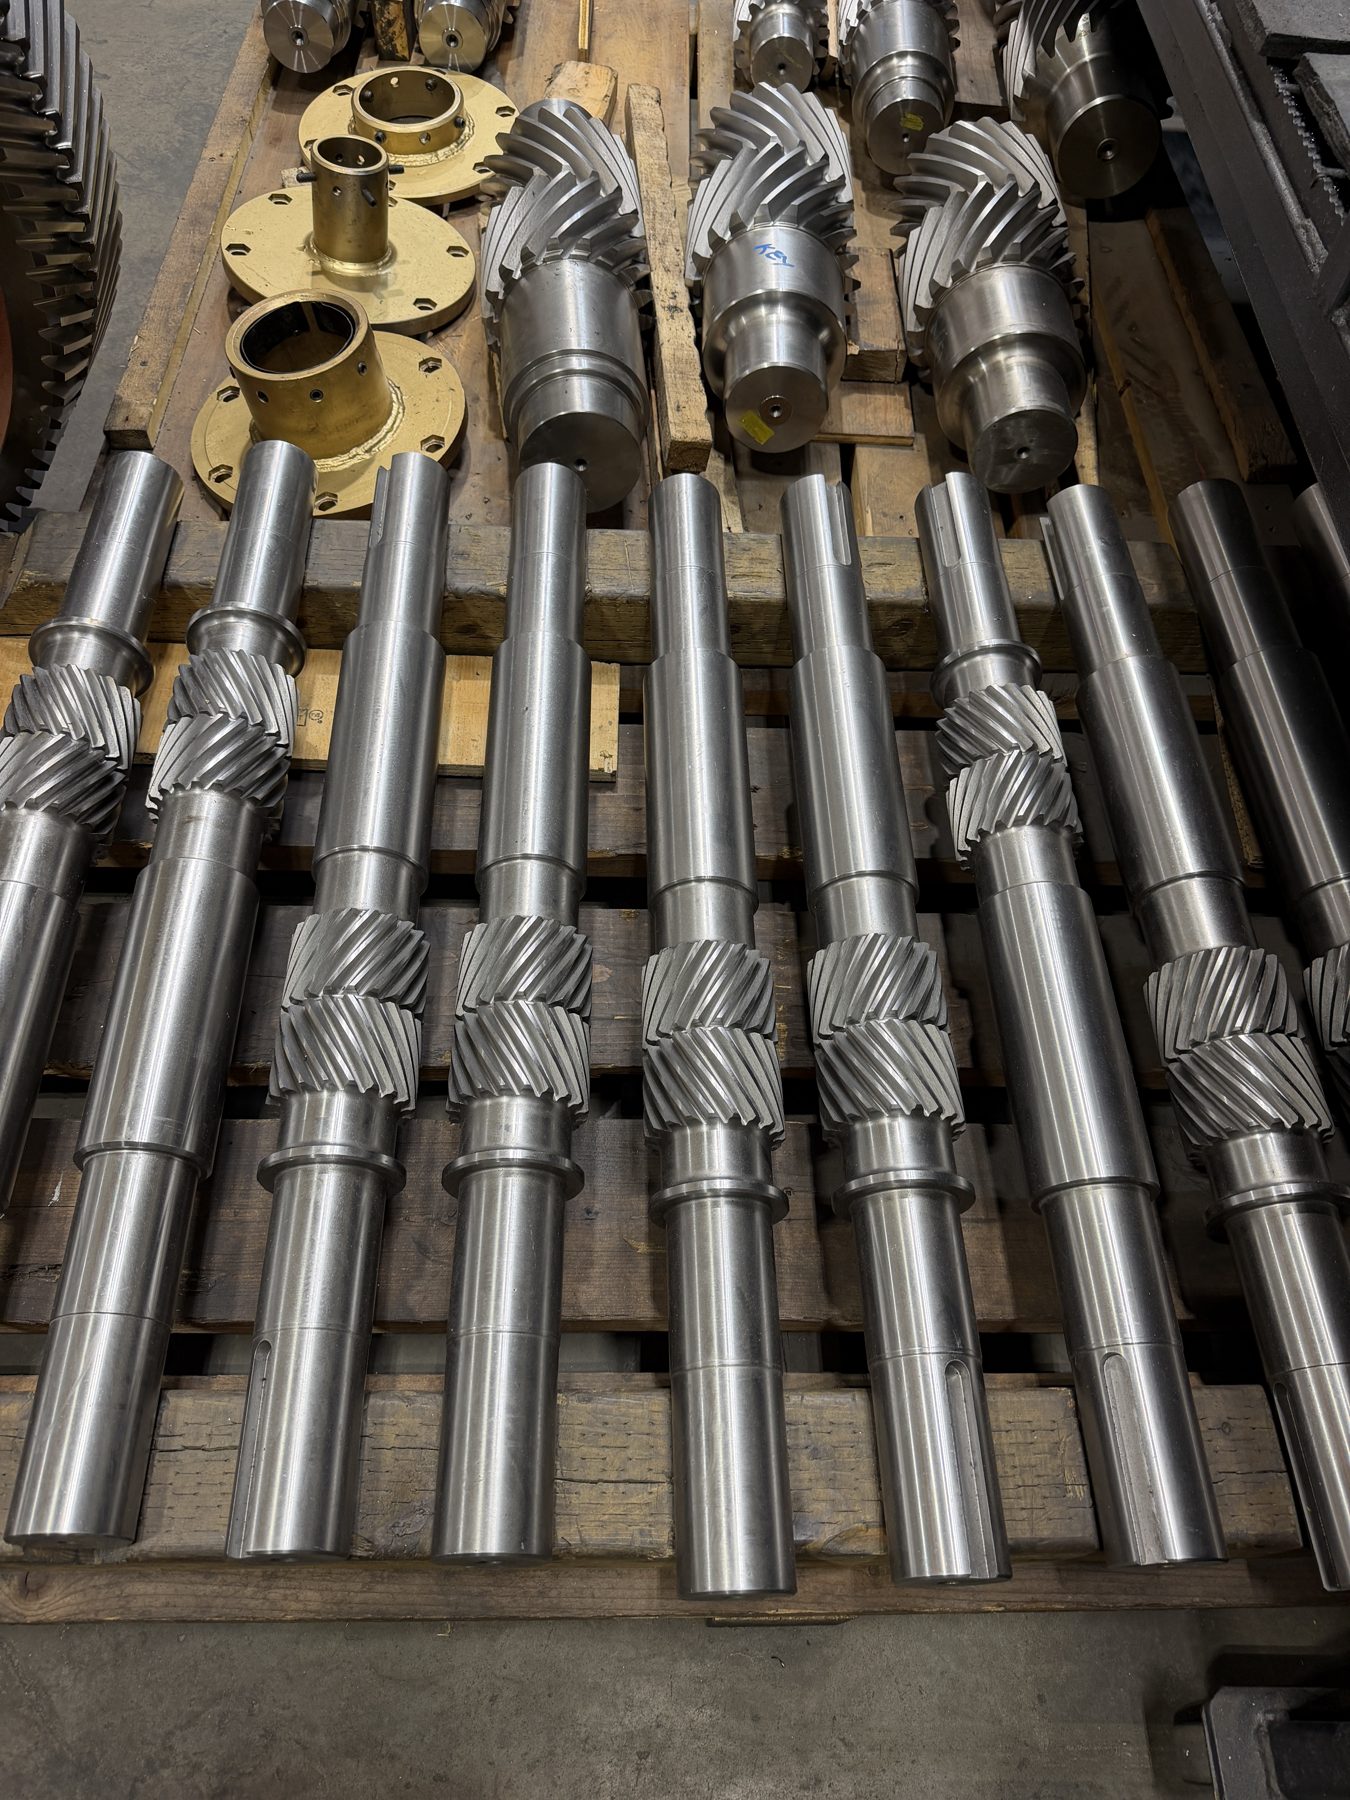
Helical pinion shafts
PinionsHelical pinion shafts
Service 01 · Specialty

Gear Cutting

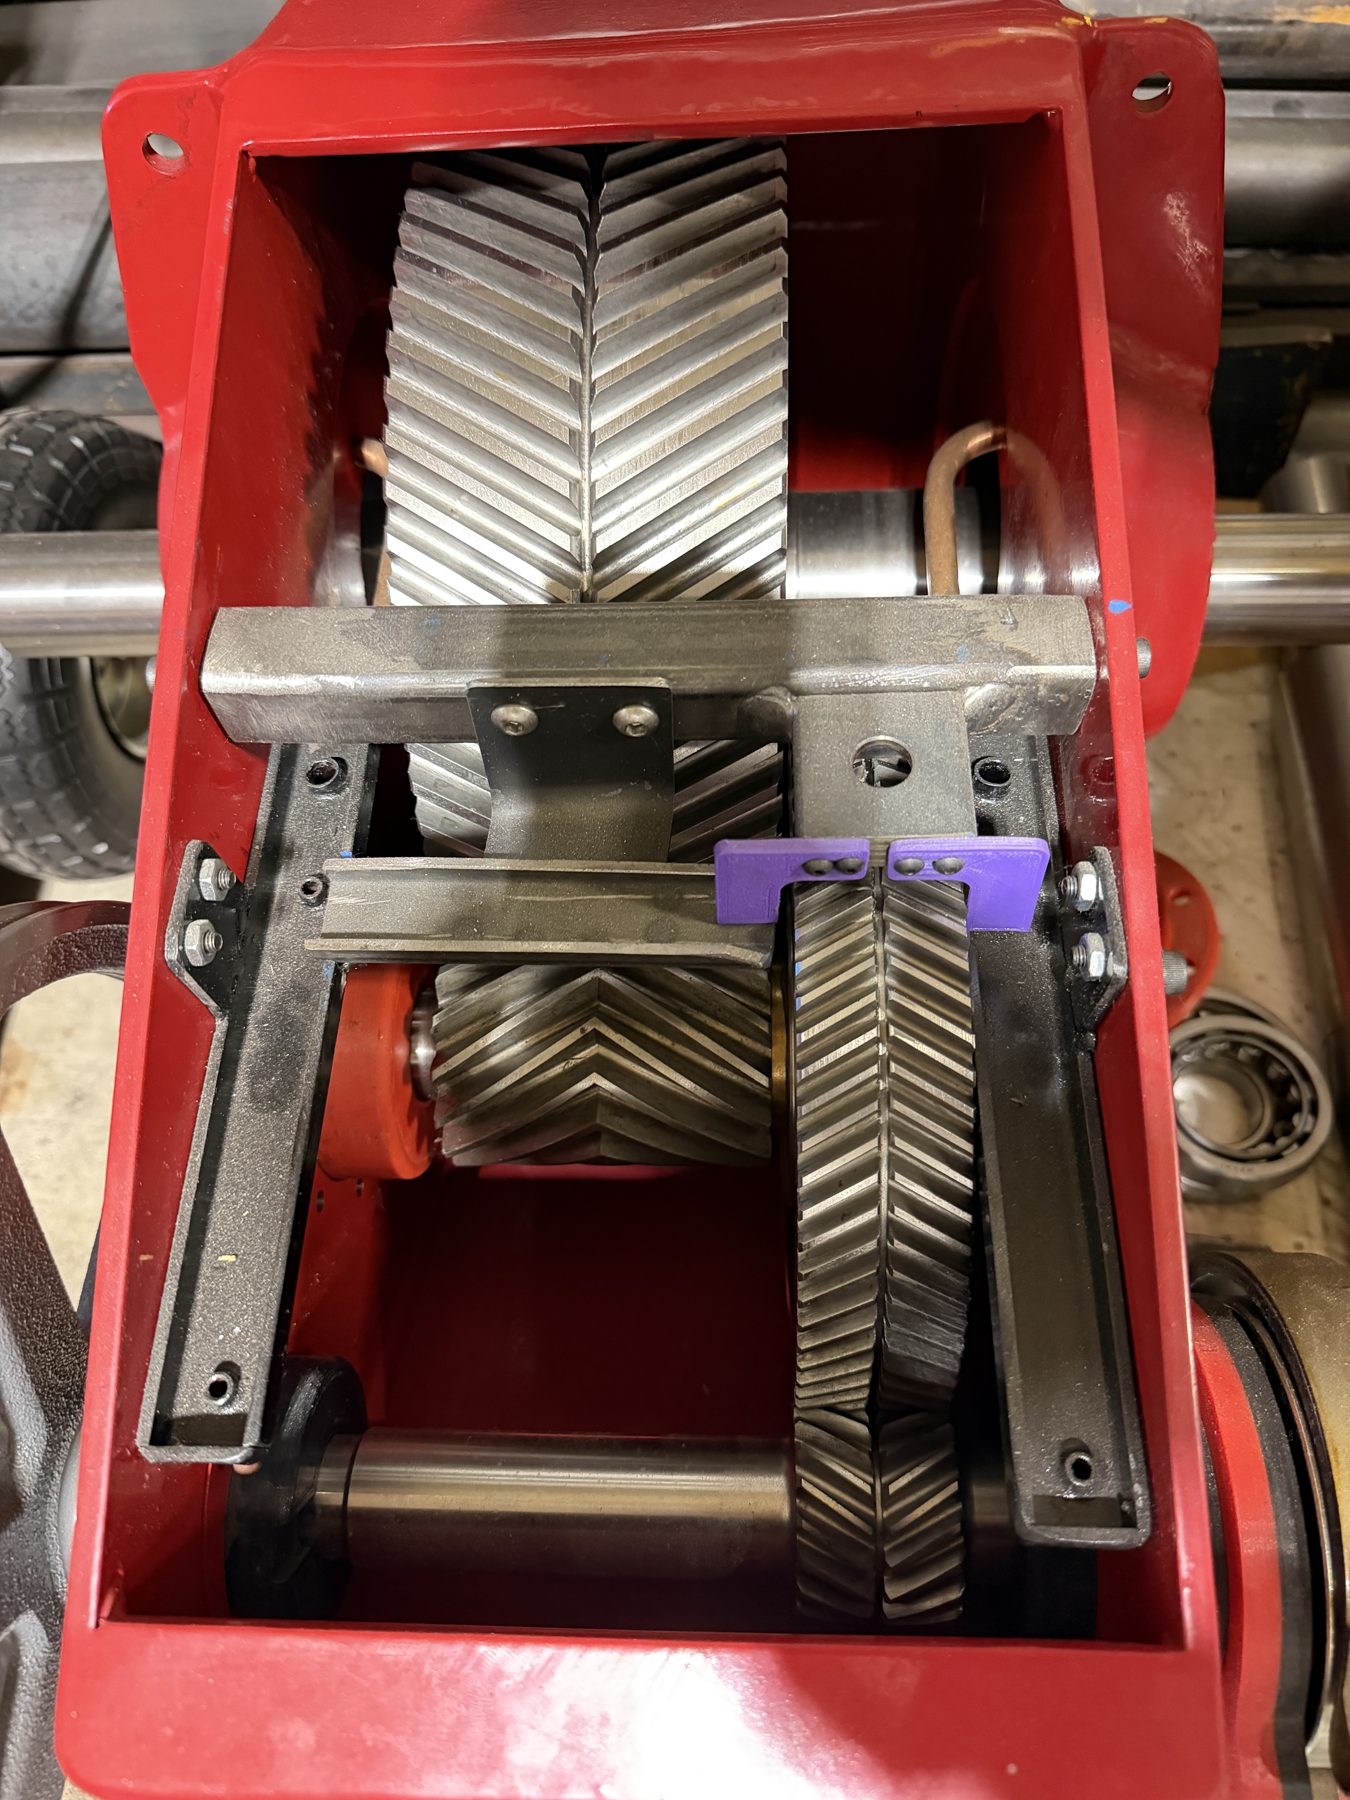
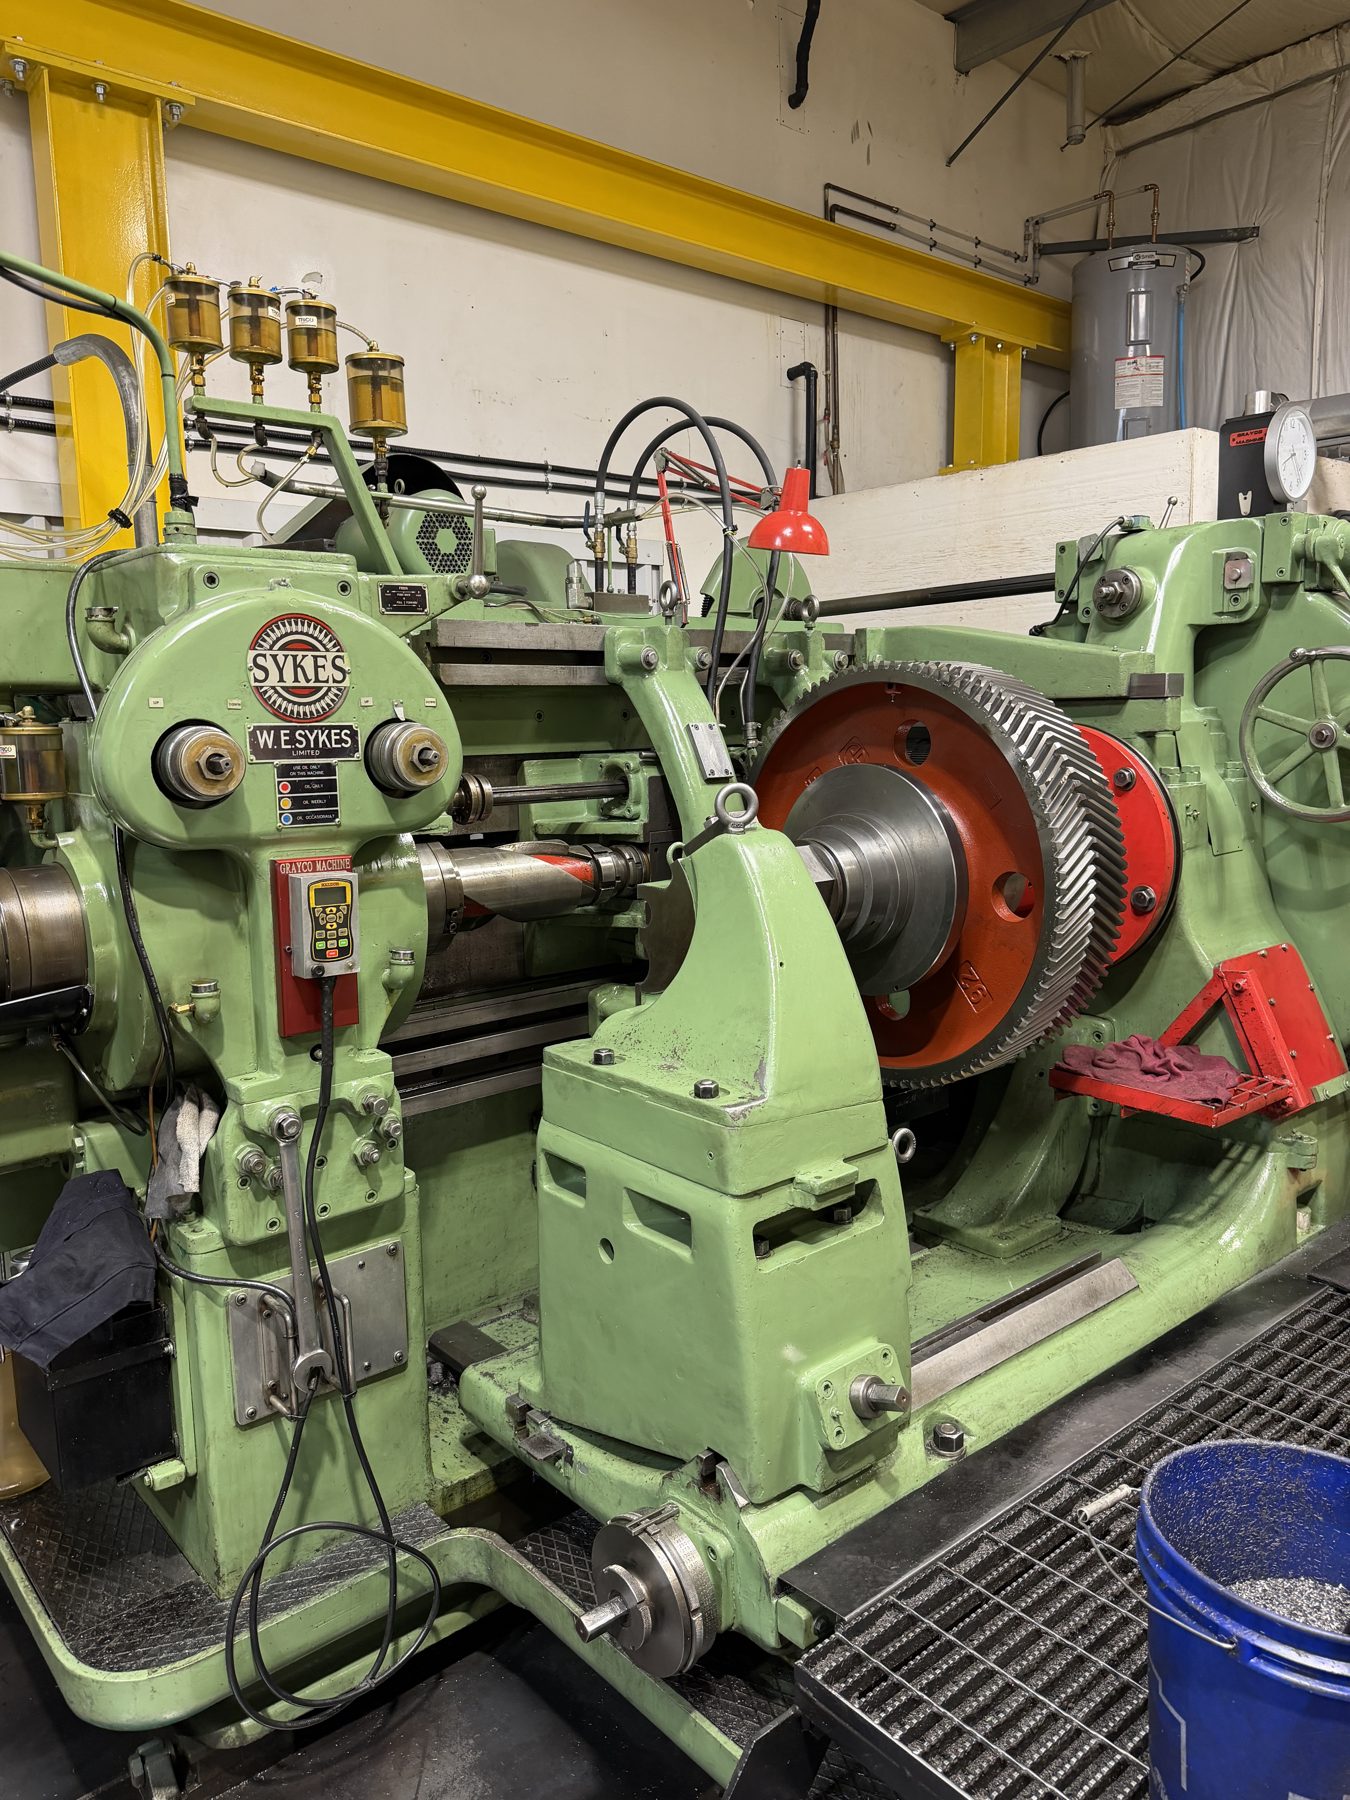
Grayco runs W.E. Sykes gear generators, the machines built to cut true solid-apex herringbone gears: continuous double-helical teeth that meet in the middle with no centre groove. The opposing helix angles cancel out axial thrust, so the gears run smoother and carry heavier loads than spur gears of the same size.

We run three Sykes machines (size 3 and size 5) and cut herringbones up to 62" OD and 18" face width, including 30° helix angles. A Lyndex-Nikken 4th-axis setup on our CNC mill adds high-end gear milling, and the wire EDM cuts internal splines and teeth. That covers almost any gear a customer needs.

Herringbone capacity
Up to 62" OD × 18" face
Sykes generators
3 machines, size 3 & size 5
Recent work
3.25 module, 15° helix sets · Taro 160 HS/LS pinions
Also cut
Spur, helical, racks, planetary, splines
  • Solid-apex herringbone
  • Double-helical gears
  • Spur & helical gears
  • Gear racks
  • Planetary pinions
  • Internal & external splines
Quote a Gear
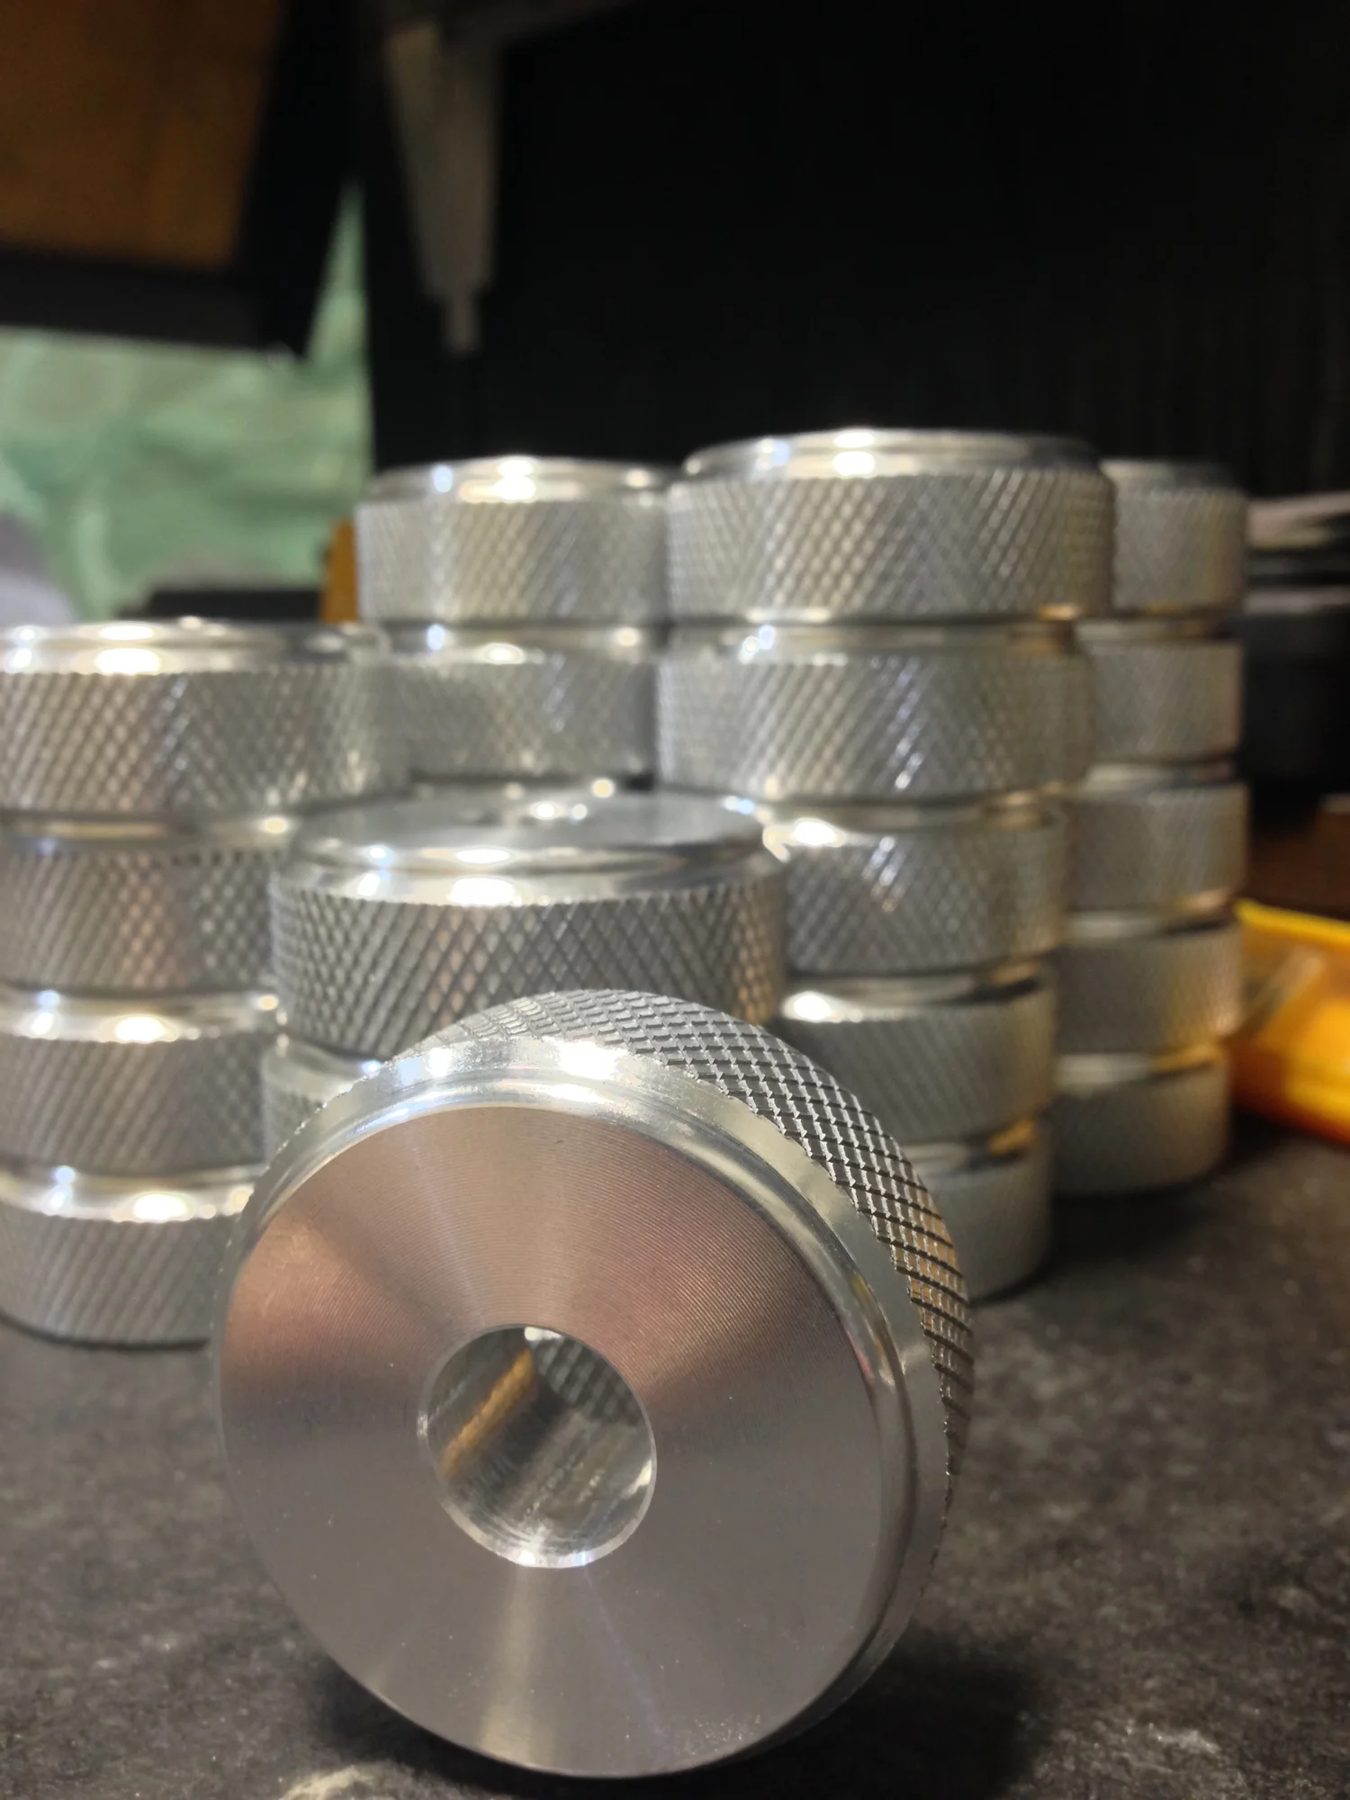
Knurled aluminum parts
ProductionKnurled caps
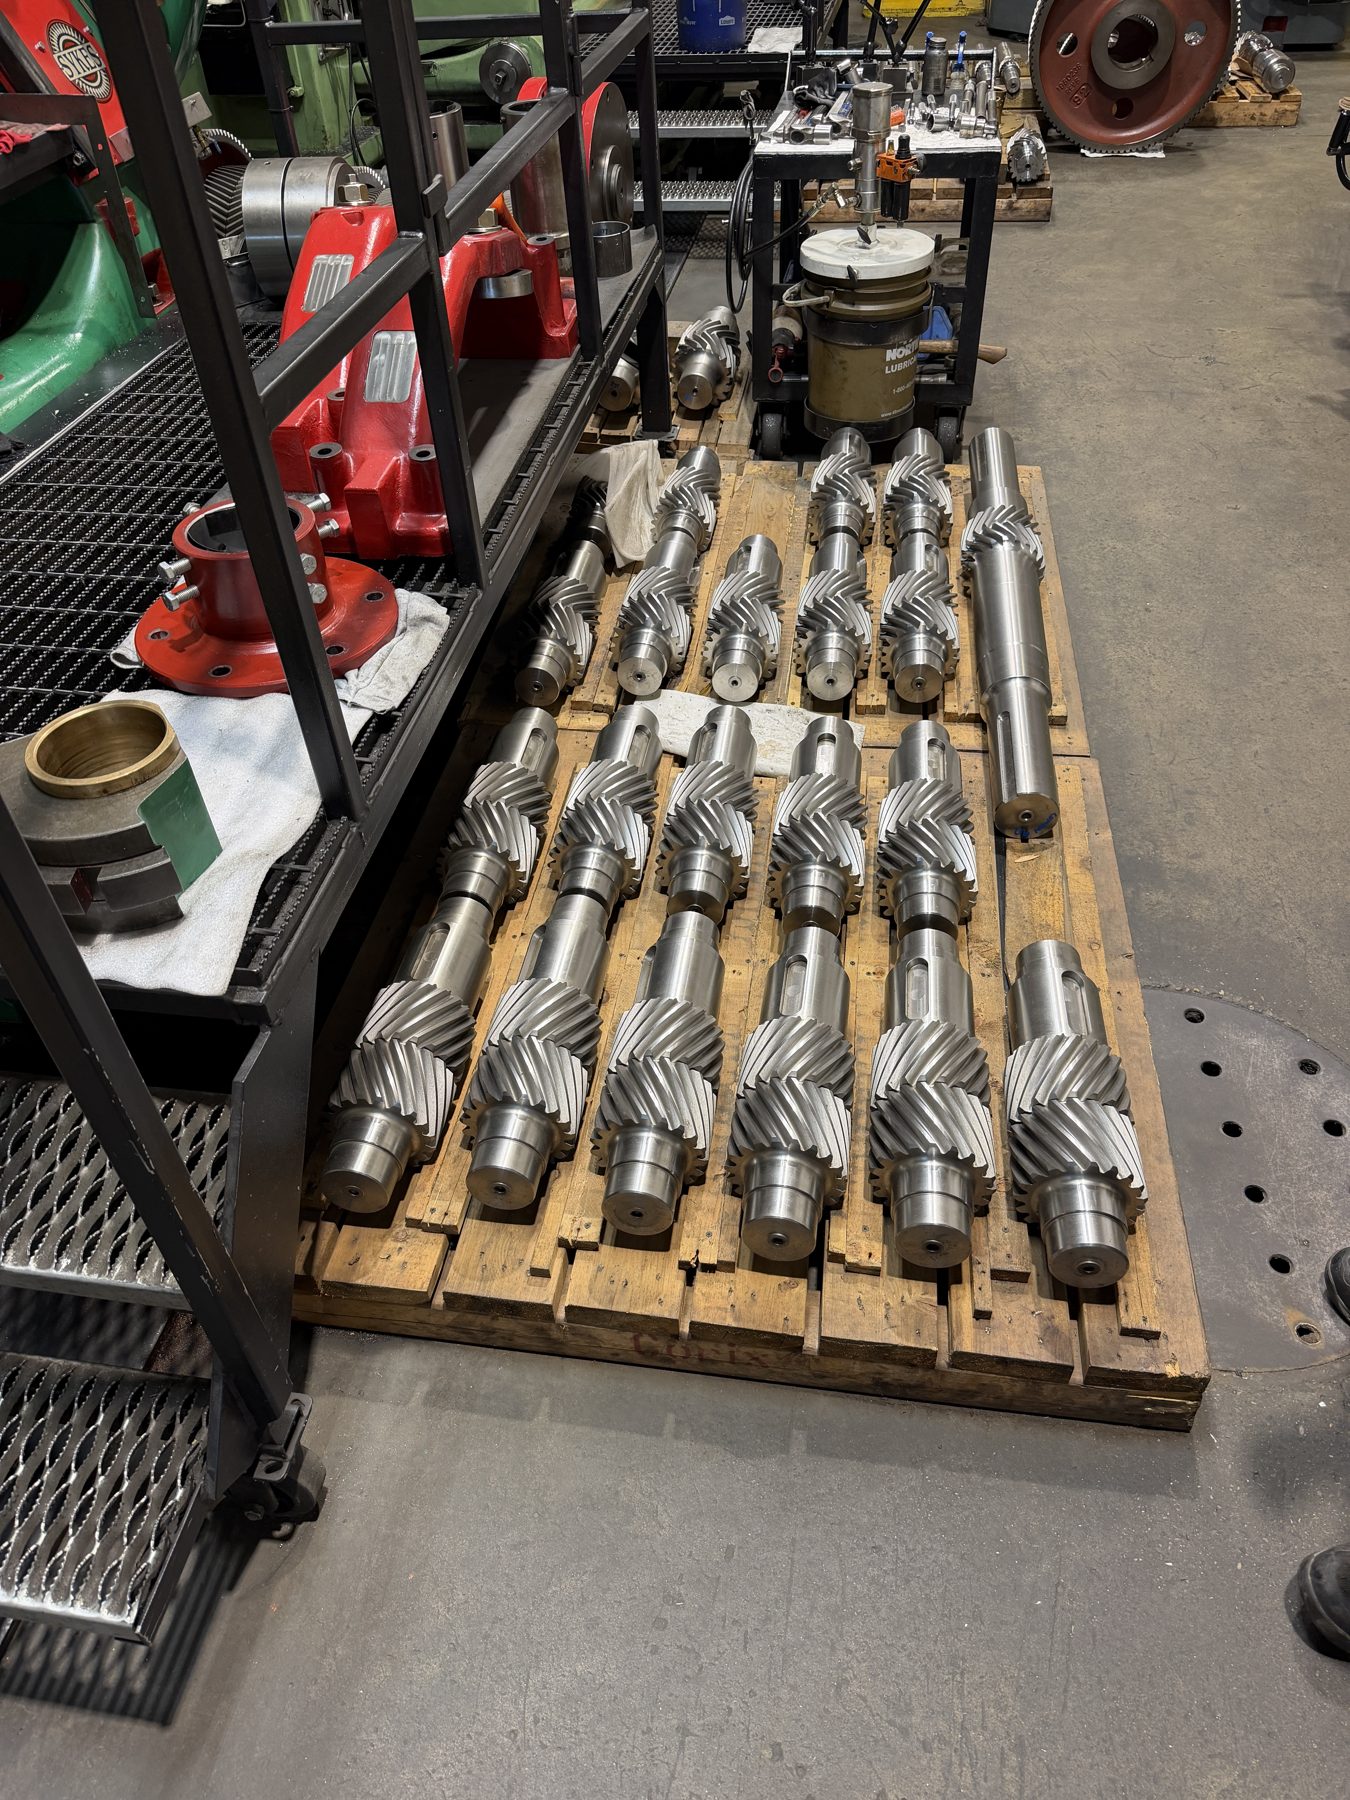
Pallet of pinion shafts
ProductionPinion shafts staged for delivery
Service 02

Production & Fabrication

Once a part is proven, we'll run it again and again: pinion shafts, pump jack tail bearing assemblies, knurled parts for sampling tools, and turned components. We also take on larger fabrication jobs, like thousands of drilled pieces welded into assemblies, and build complete products such as forage samplers, scraper blades and pipe-bursting tools.

  • Prototype to production
  • Repeat orders
  • Machined weldments
  • Multi-process parts
Quote a Production Run
Herringbone gears in gearbox
GearboxHerringbone set in housing
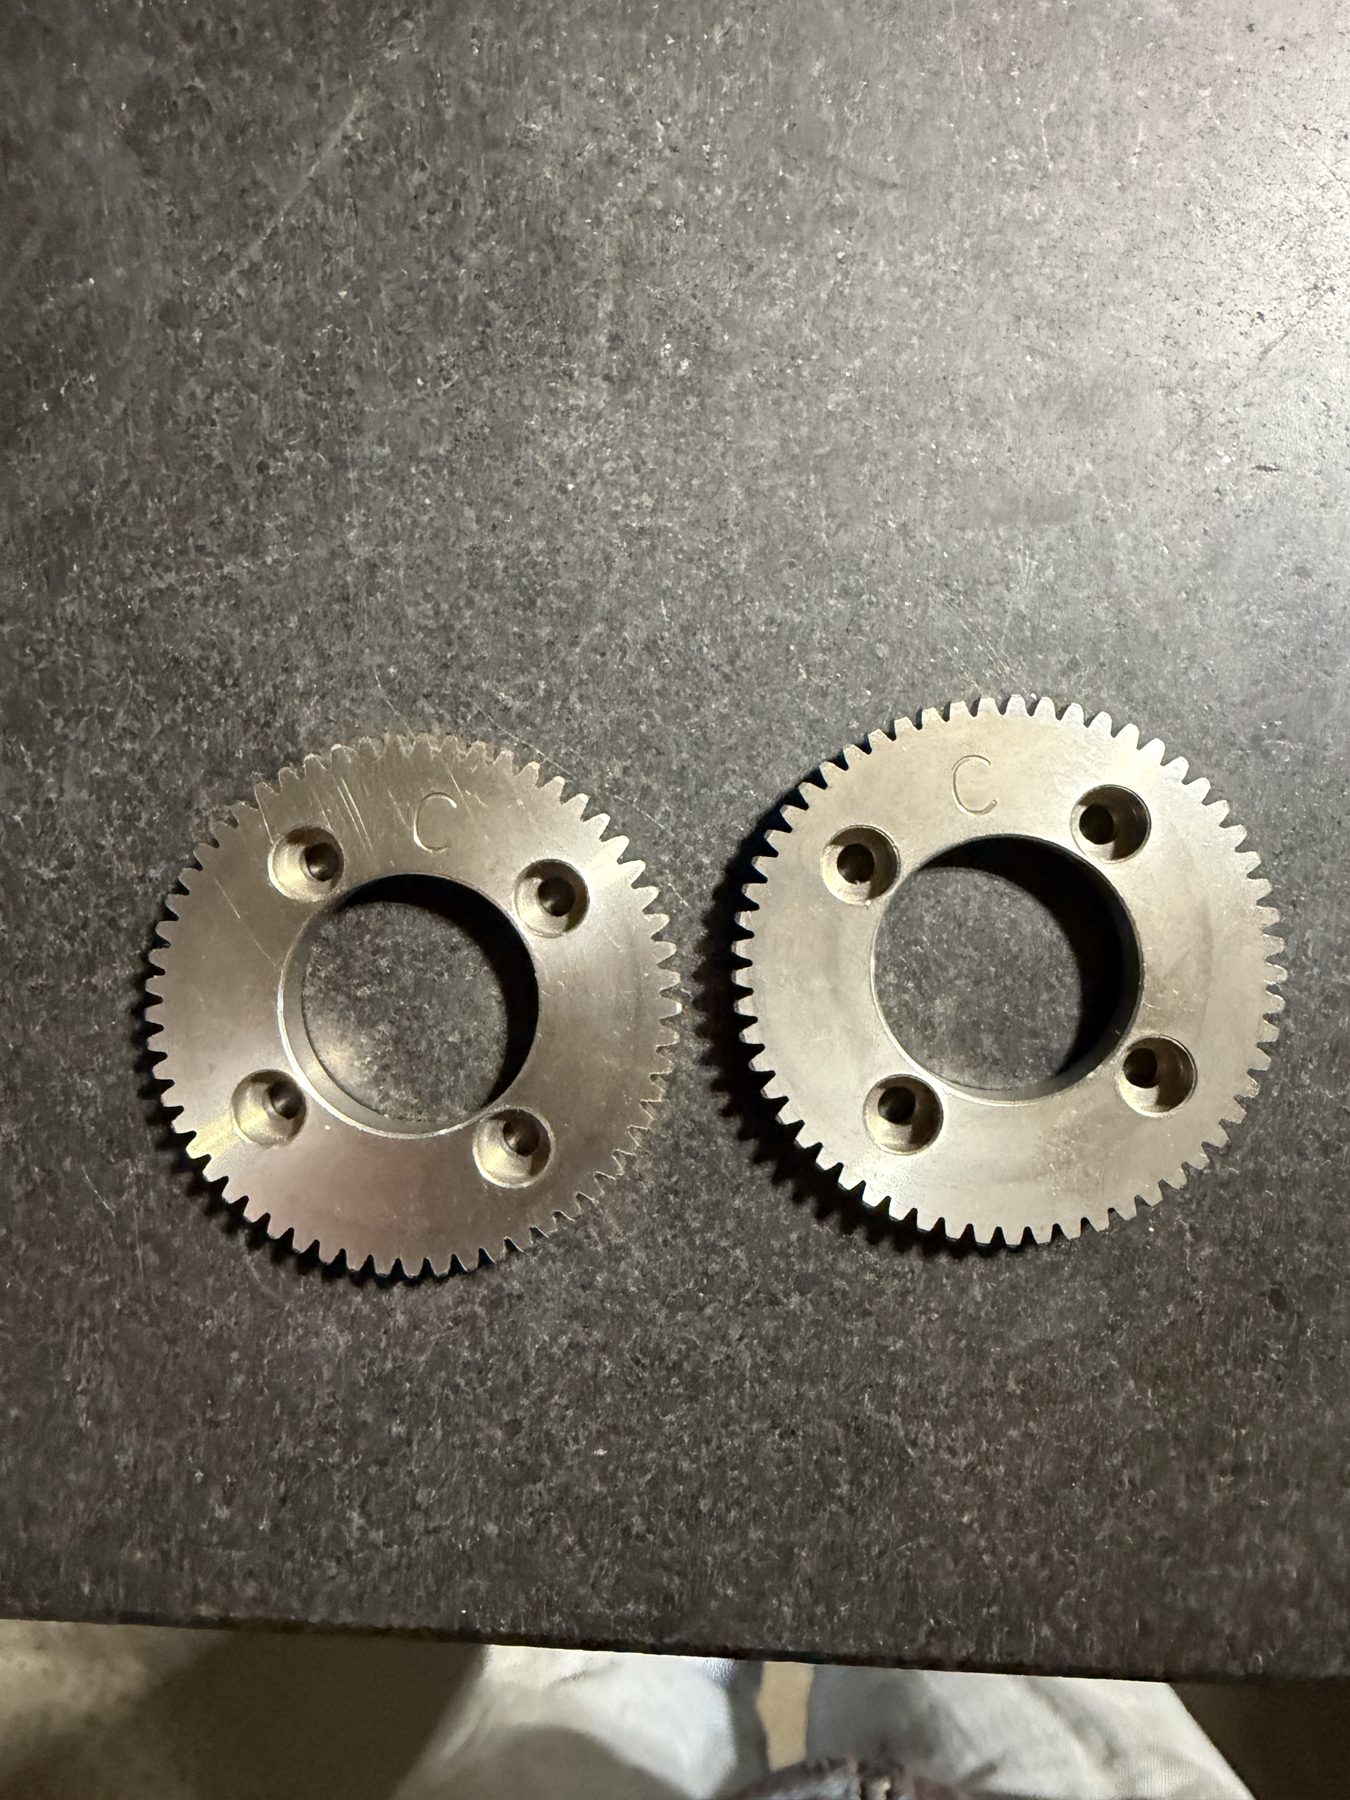
Matched spur gears
InspectionMatched to sample
Service 03

Repair & Reverse Engineering

Bring in the broken part and we'll make it the same as the sample. We measure it, rebuild the geometry, and machine a replacement, including gears and parts the original manufacturer no longer makes.

"Reverse engineering seems like a daily task around here." Past jobs include gearbox housings made to sample, a metric valve-actuator spline rebuilt in a rush, carbon brush holders a customer couldn't buy anymore, and copper contacts for a 1940s freight elevator that no one else would make. For worn gears, we can wire-EDM the old teeth and machine a matched shaft to fit.

  • Made-to-sample parts
  • Gear & spline measurement
  • Gearbox rebuilds
  • Obsolete components
Send Us a Sample
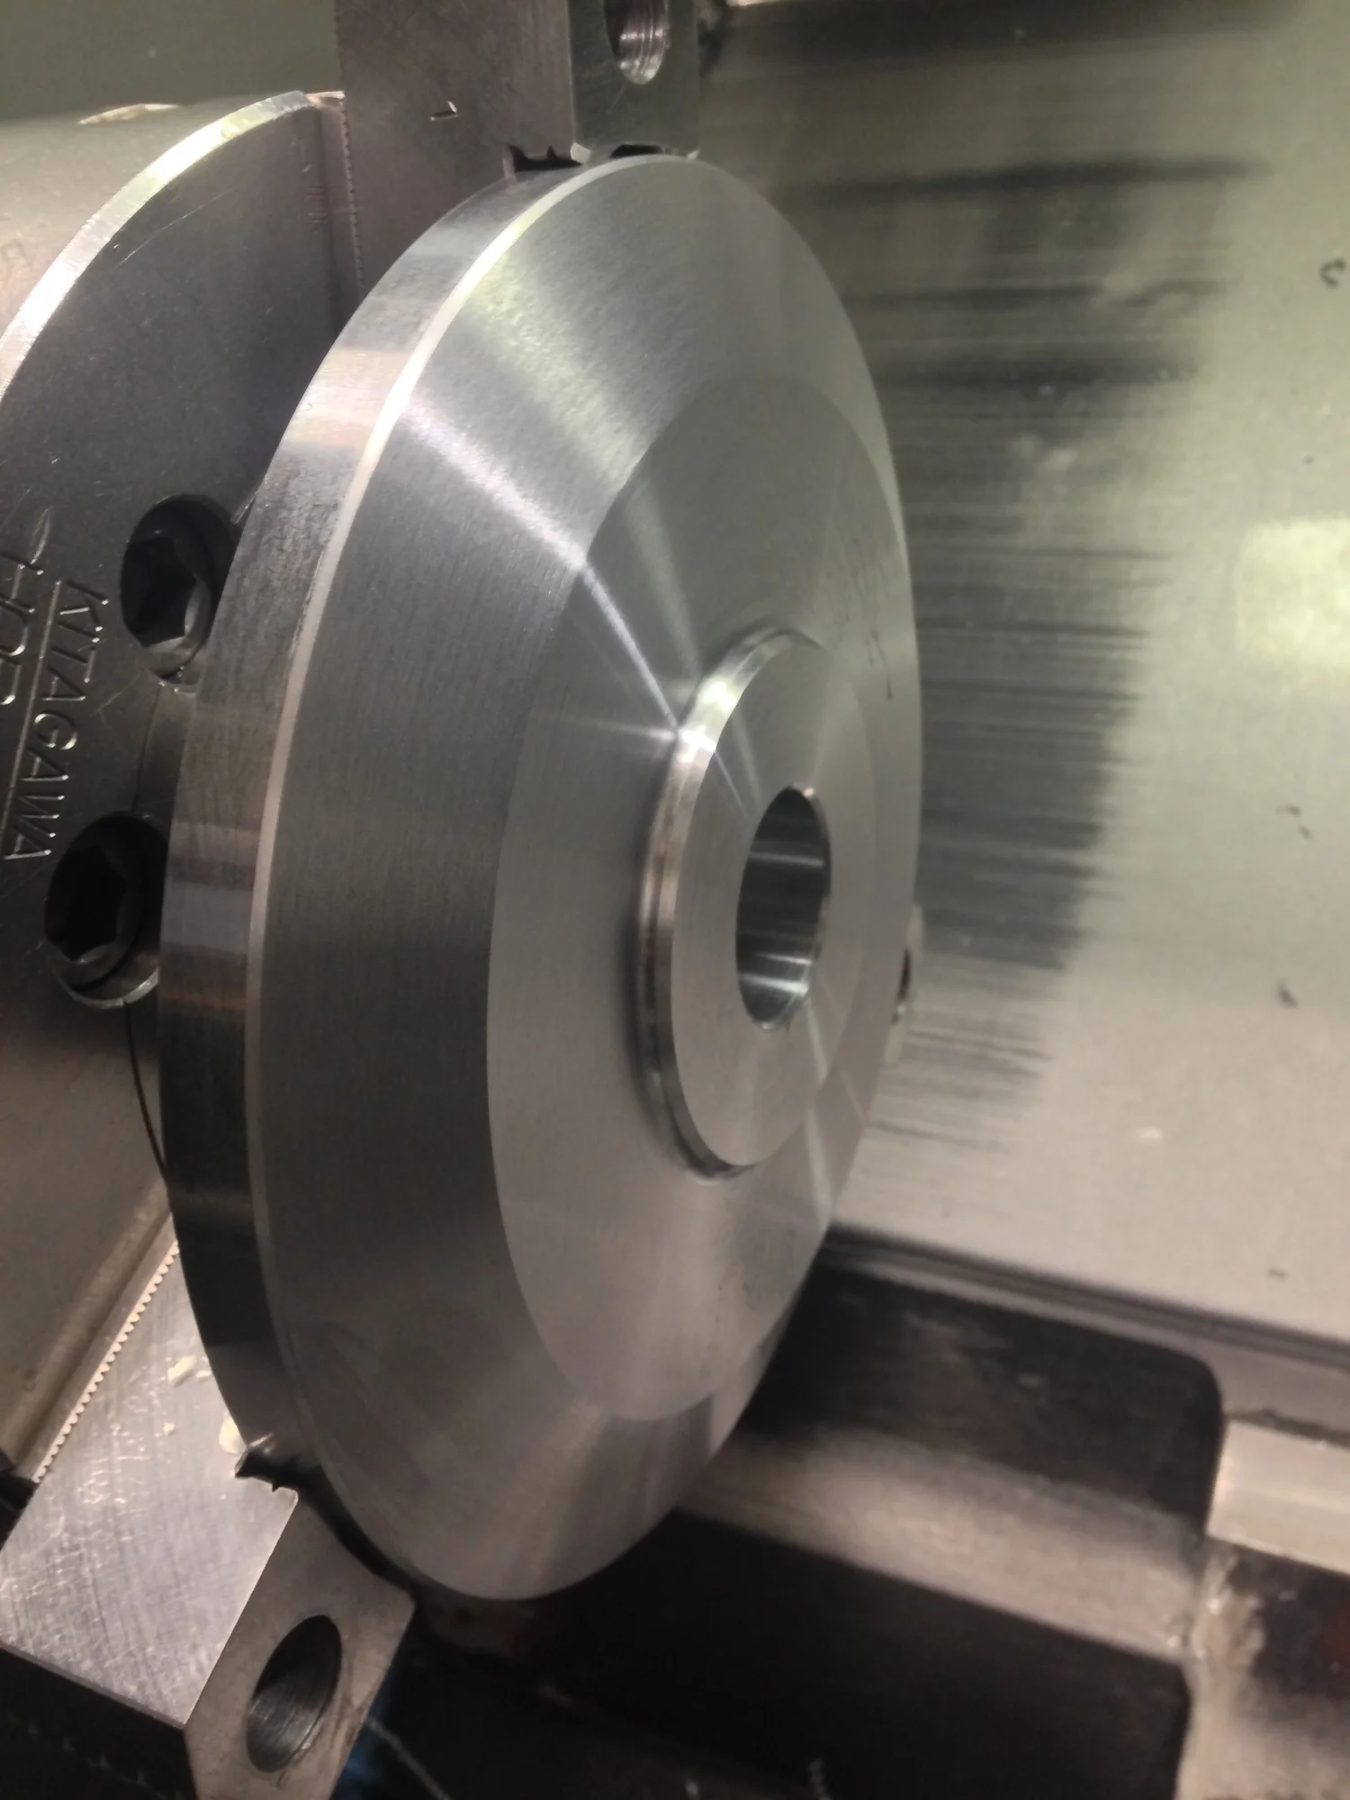
Turned flange in lathe
TurningFlanged hub
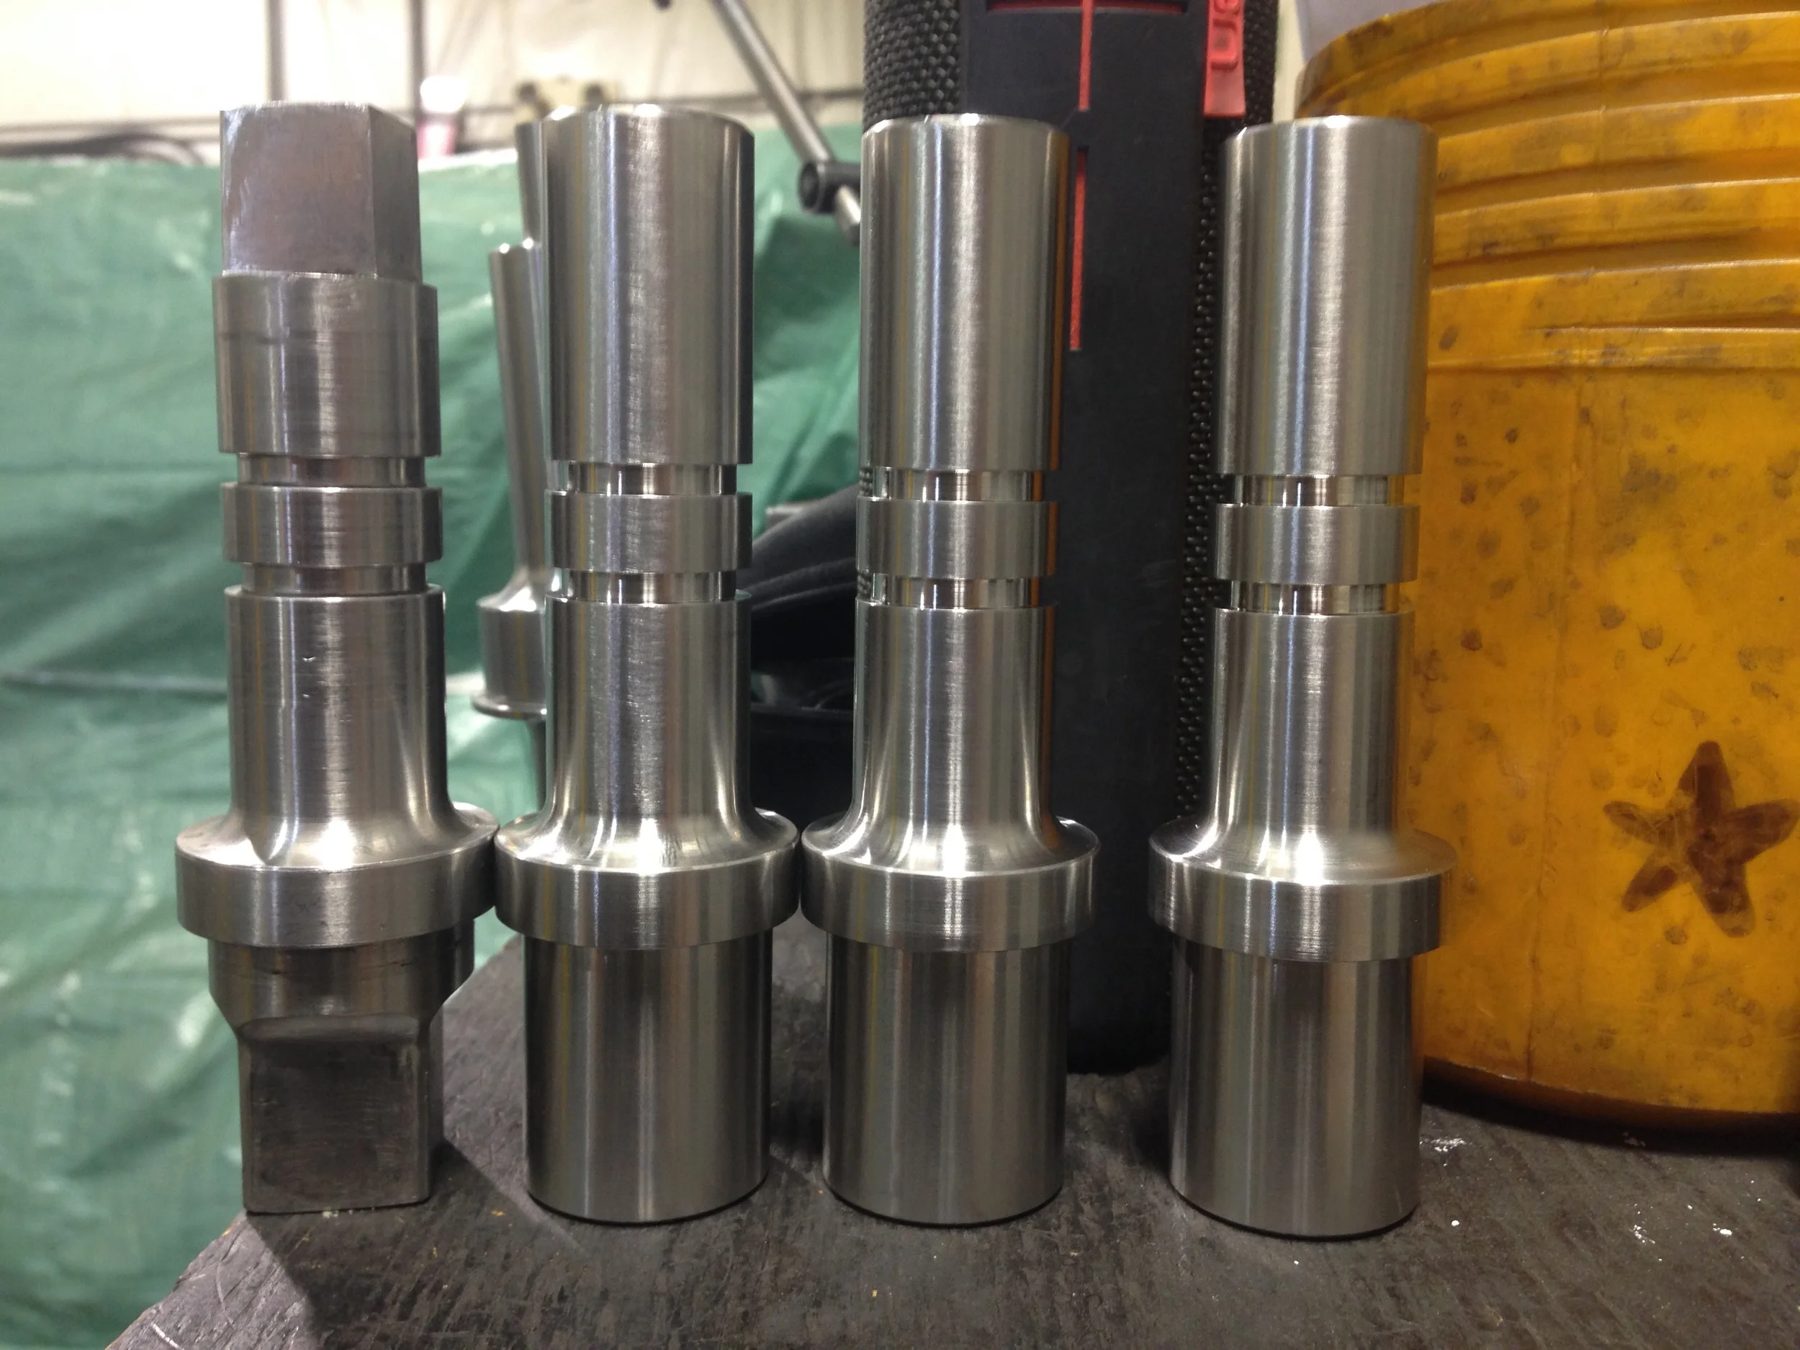
Stepped stainless shafts
ShaftsStepped stainless shafts
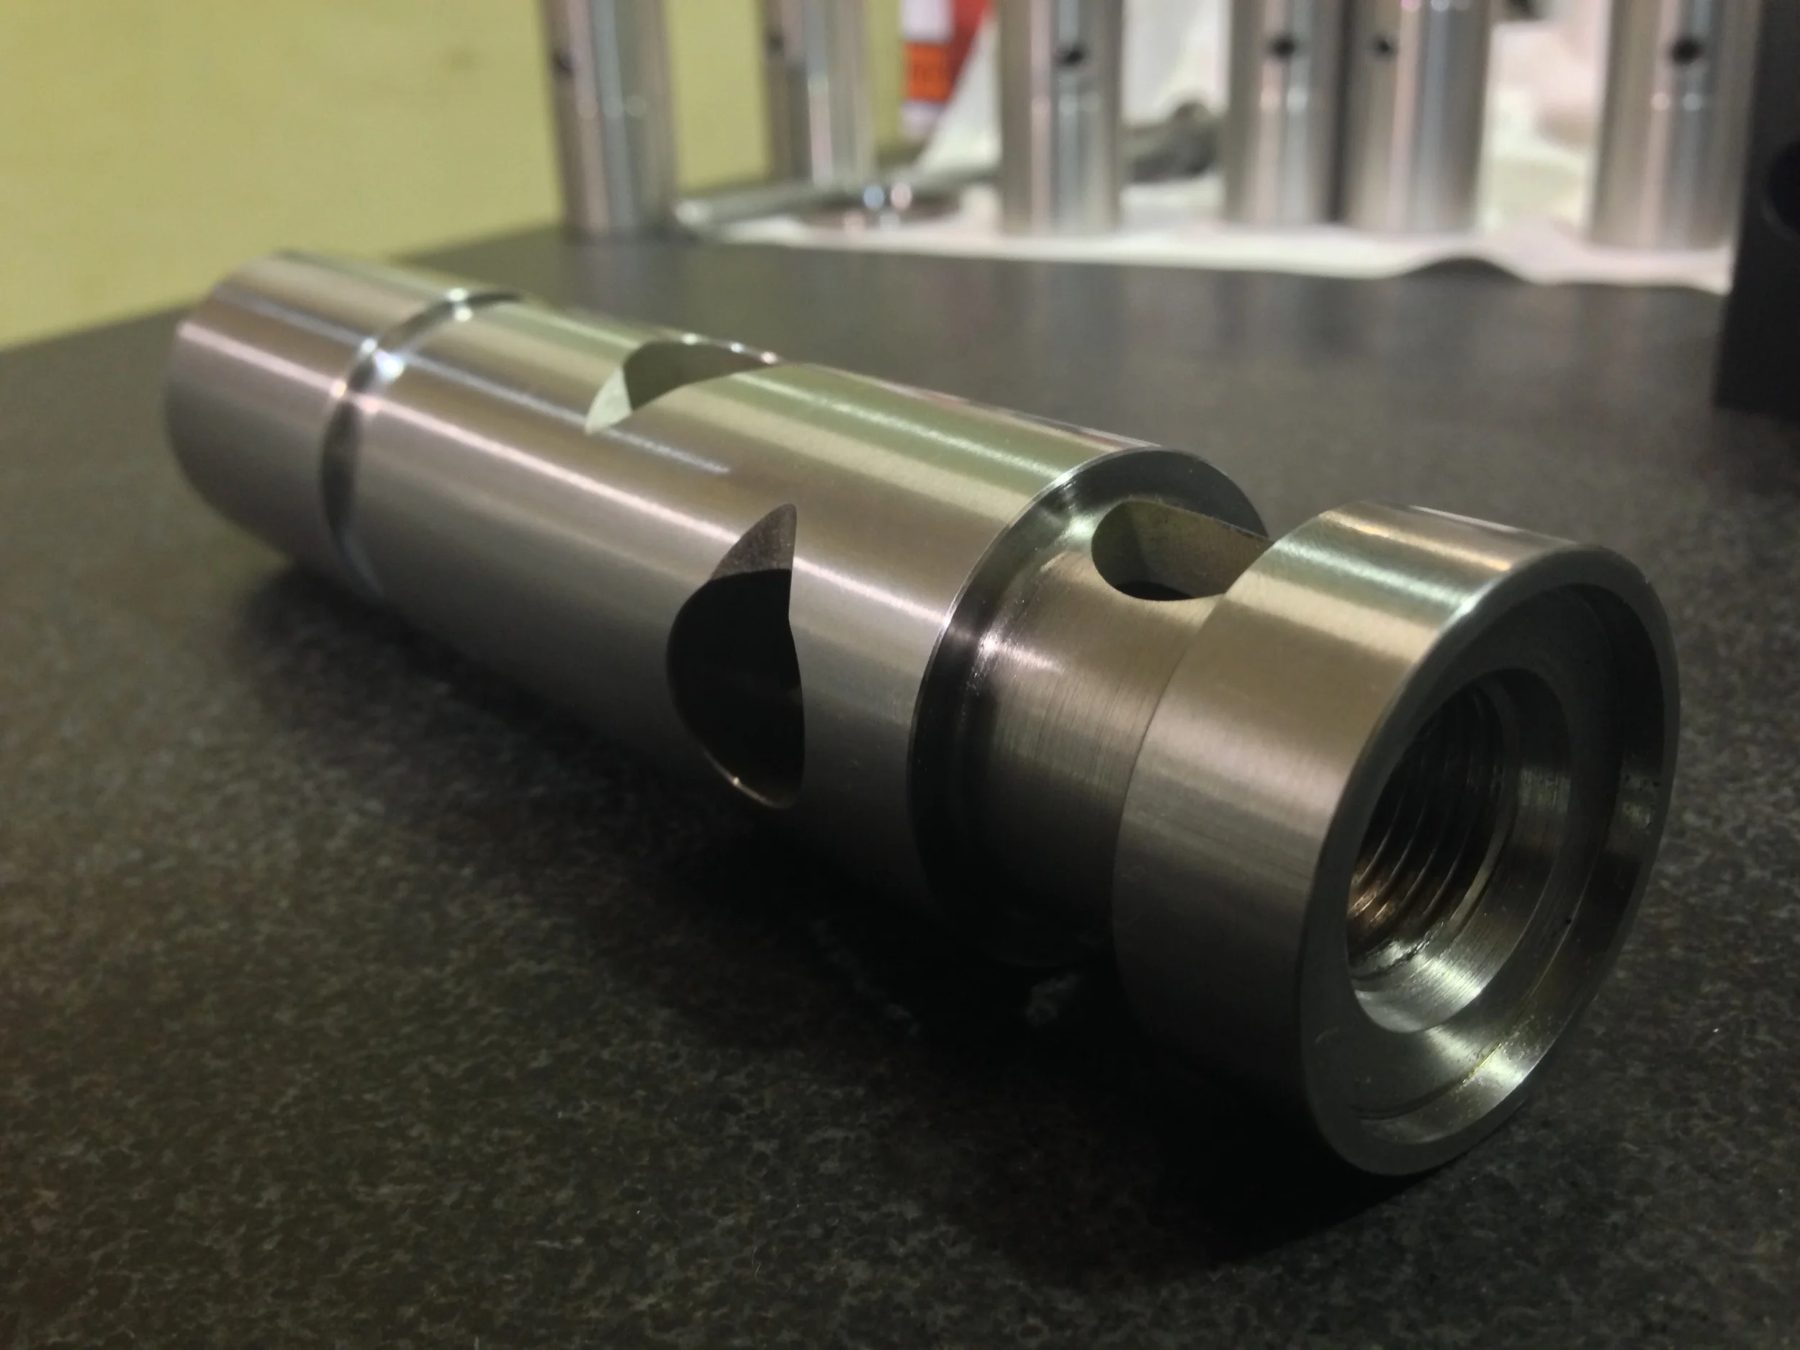
Ported stainless component
MillingPorted down-hole body
Service 04

CNC Machining

CNC turning centres, including a Hyundai WIA lathe, and a CNC vertical machining centre handle everything from one-off prototypes to repeat production. Shafts, couplings, bushings, flanges and down-hole components come off these machines with repeatable accuracy.

Every program is built in Mastercam CAD/CAM, which lets us take on complex profiles and 3D geometry that can't be programmed by hand. Examples include trochoidal roughing in 320 BHN 4145 steel, 4th-axis gear milling, and intricate impellers for down-hole tools.

Processes
CNC turning, CNC vertical milling
Surface finish
64 Ra → 8 Ra
Materials
Alloy & tool steel, stainless, aluminum, bronze
Programming
Mastercam CAD/CAM
Quote CNC Work
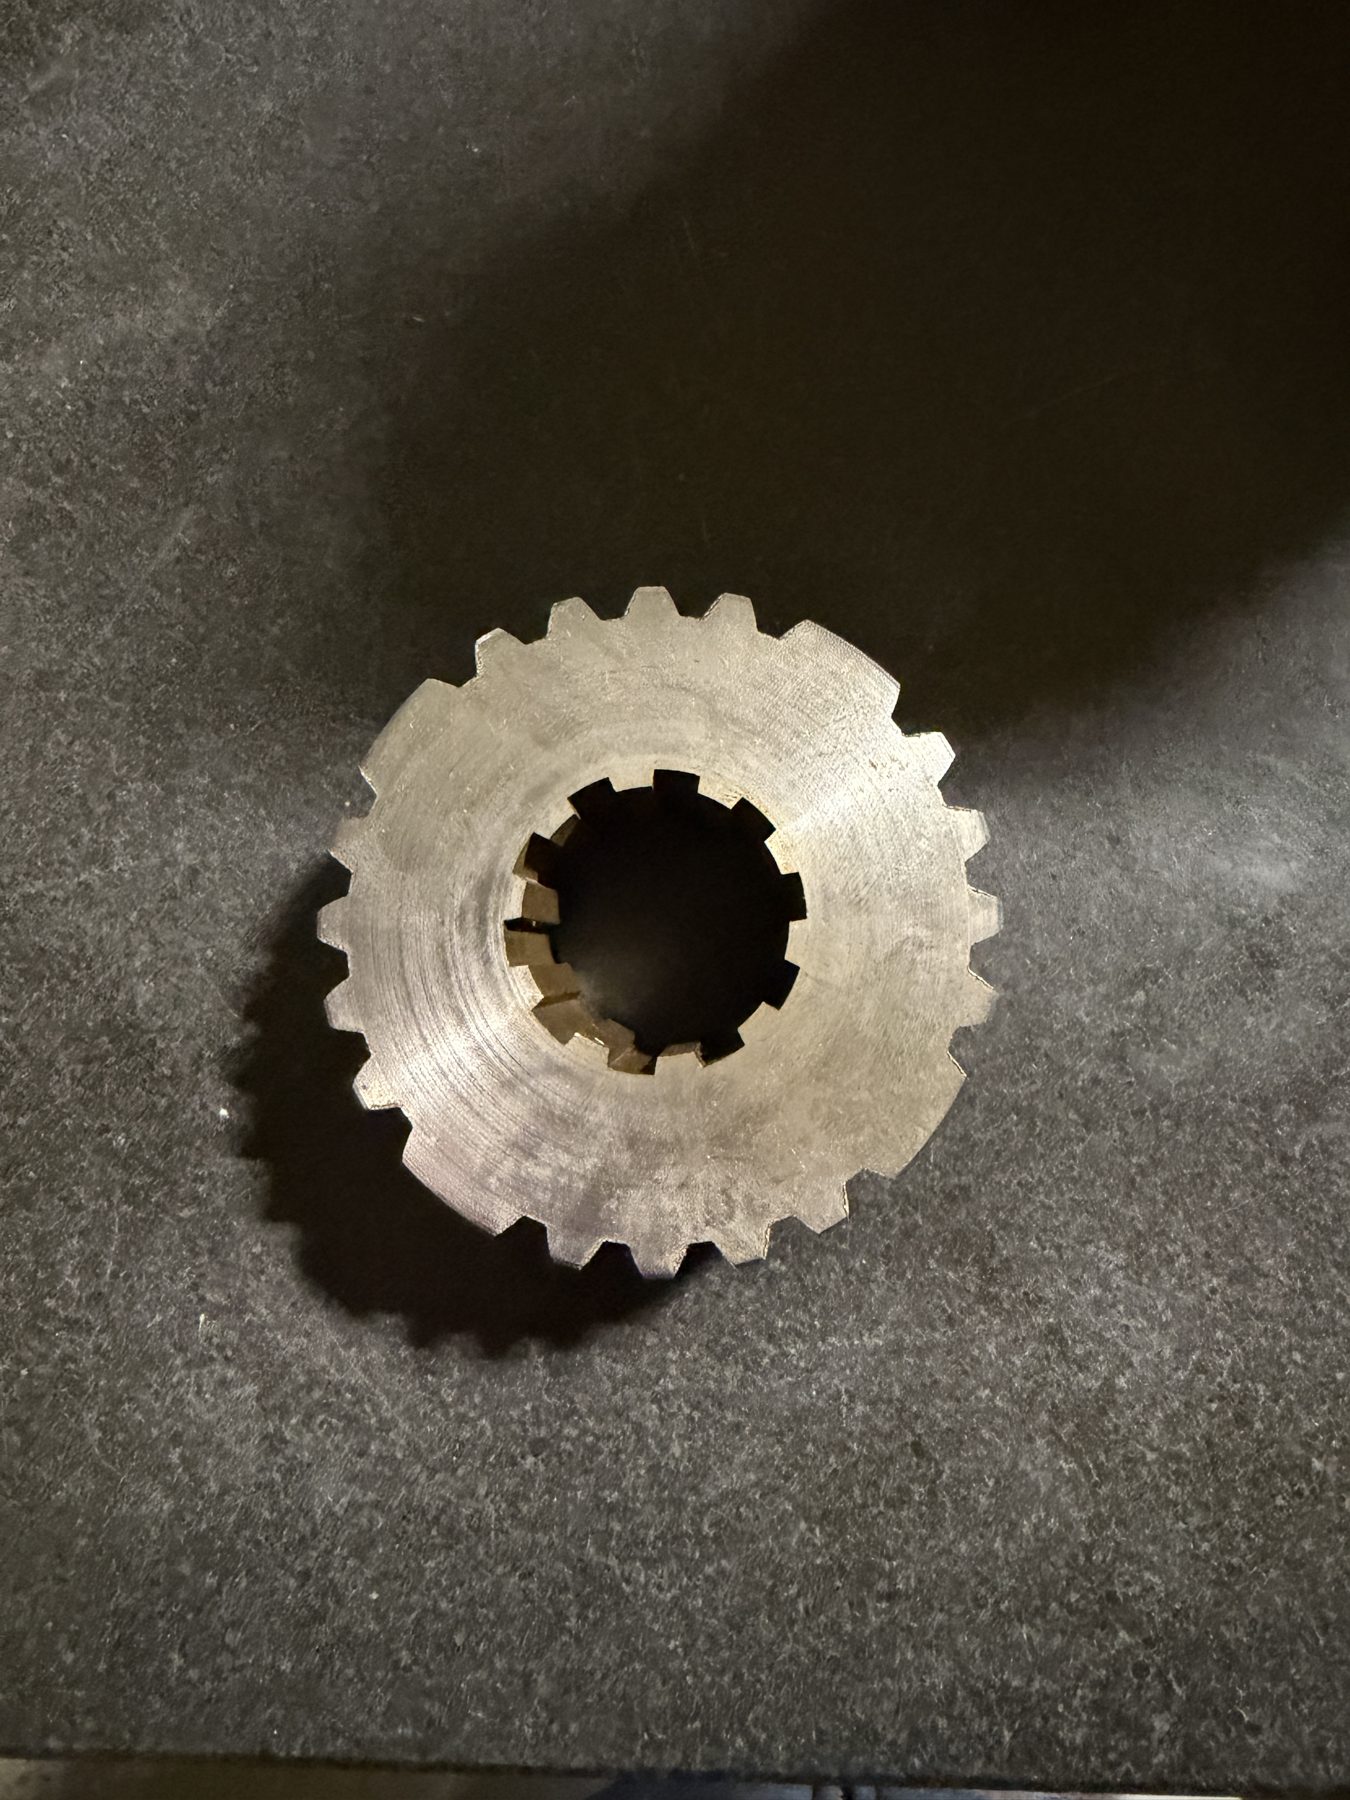
Internal spline gear
SplinesInternal spline
CNC and EDM bay
Shop FloorCNC & EDM bay
Service 05

EDM

Electrical discharge machining cuts hardened steel and exotic alloys with no cutting force, so it reaches sharp internal corners, keyways and forms that a tool can't. Grayco runs all three EDM processes in-house.

Typical EDM work: internal splines, a 5" metric keyway burned to a shoulder, 60° tapered grooves, solid-carbide grooving inserts, and holes as small as .010" through a 4 mm set screw. The most complex was a 30" custom air chuck, stellite-welded on every face and finished on our CHMER EDM, with compound angles throughout.

Wire EDM
CHMER. Profiles, keyways, tight internal corners
Sinker EDM
Blind cavities, internal splines, burned forms
EDM drilling
Small, deep start holes and through-holes
Materials
Hardened tool steel, stellite, exotic alloys
Quote EDM Work
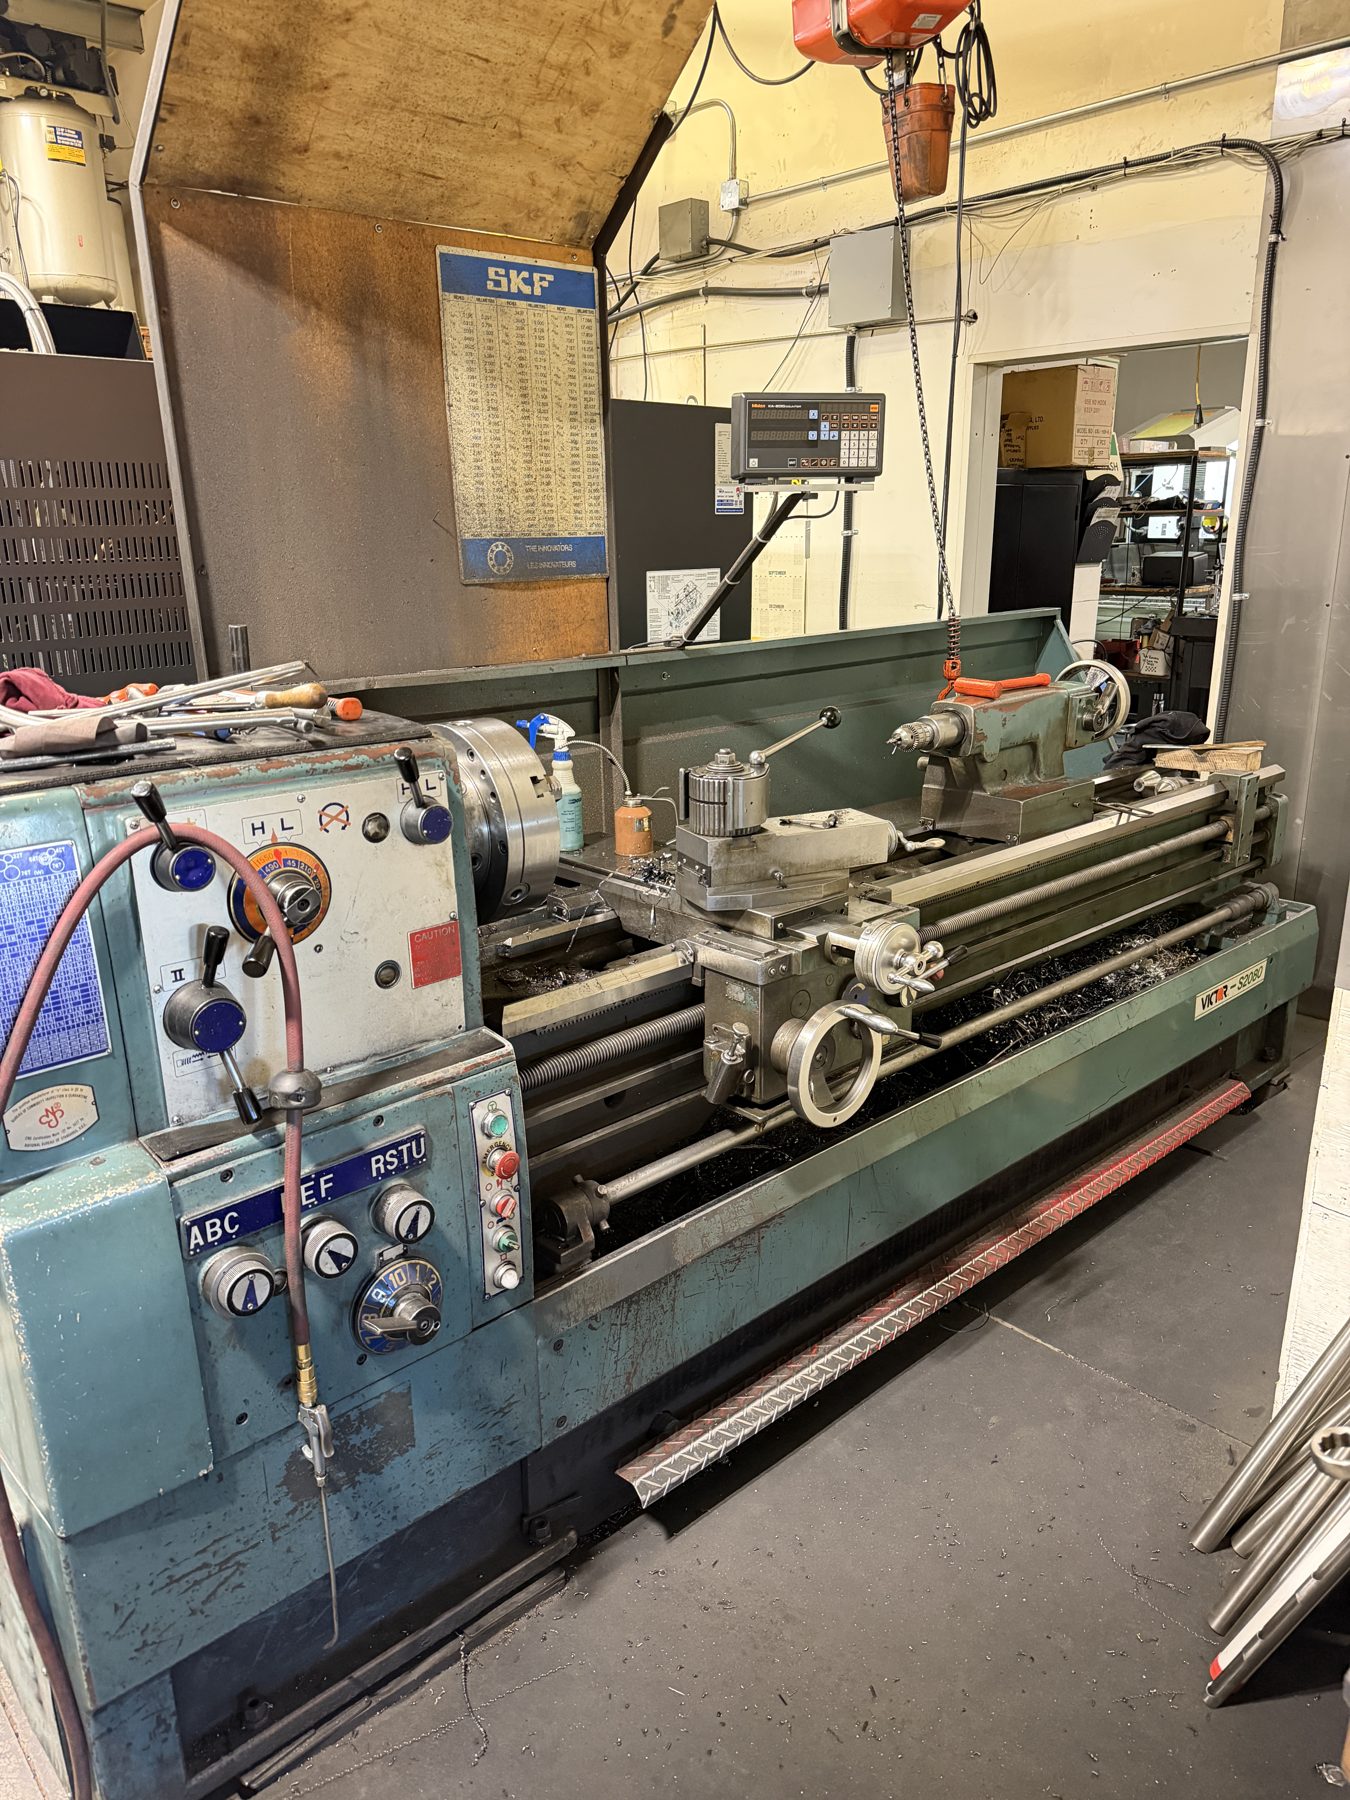
Large manual engine lathe
ManualLarge-swing engine lathe
Service 06

Manual Machining

Not every job needs a program. Our large-swing manual lathes and mills are the fastest route for one-off parts, long shafts, heavy work and breakdown repairs where a machine needs to be back in service today.

  • One-off & rush parts
  • Long shafts
  • Bushings & sleeves
  • Keyways & fits
Quote Manual Work

Have a print, a sample, or a broken part?

Send it to our Leduc shop. We'll review the job and get back to you with a quote. Serving Edmonton, Nisku and all of Alberta.

Call Get a Quote